
Steam hose maintenance comes down to five practices: store the hose so it cannot take a set, check it before every shift, control the warm-up, drain condensate at both ends of the run, and retire on evidence rather than on failure.
This guide works through those five practices in the order a plant actually performs them. It covers what a hose needs between shifts, which checks find trouble before it becomes a leak, and why steam admission is the most destructive minute of a hose’s day. It also shows how a simple record turns good habits into a program that survives a shift change. Every point is written for the person holding the hose, not for the file cabinet.
Pressures are gauge pressures. Steam temperatures are the saturation temperature at that pressure, so they move with the pressure and cannot be chosen independently. About 17 min read.

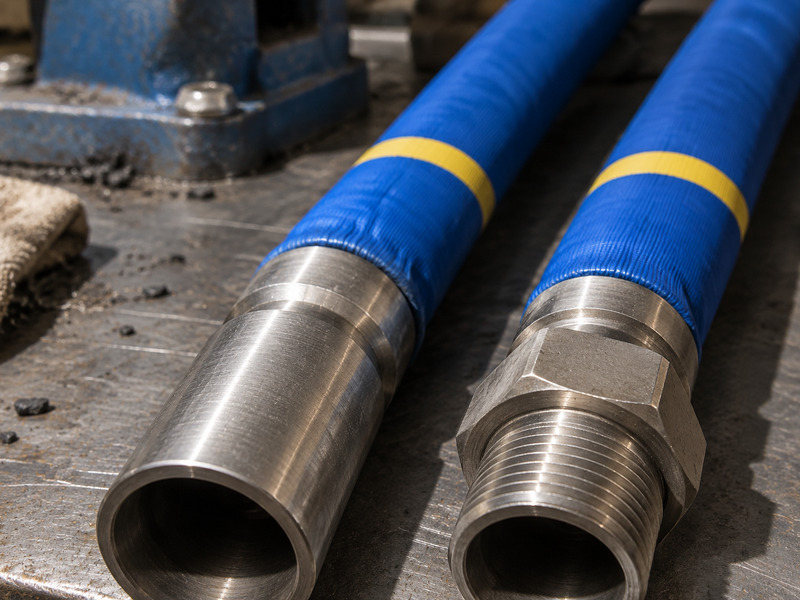
Figure 1. A steam hose between jobs: supported, off the floor, with both ends visible so the next shift can inspect it before it is put back into service.
Scope: the five practices in this guide apply to rubber steam hose carrying saturated steam and its condensate, with the duty inside the hose rating. Superheated steam is a different duty, and it needs its own specification review before these practices apply.
What Steam Hose Maintenance Actually Involves
Steam service is harder on a hose than most duties in the same plant. The tube sees hot water, saturated steam and condensate within a single working day, and each of those three media attacks it differently. Condensate is the most aggressive at the tube wall. Dry saturated steam is easier on the rubber, but whatever permeates the wall has to leave through the perforated cover, and until it does it sits against the reinforcement.
Steam hose maintenance is therefore not one task but five, and each repeats on its own clock:
- Between jobs — storage, support and protection from sunlight, ozone and oils.
- Before every shift — a short visual and hand check of the cover, couplings and restraint.
- At start-up — a controlled warm-up before full steam admission.
- At shutdown — drainage of condensate from the hose and from the line that feeds it.
- At end of life — a written replacement decision, based on findings rather than on a leak.
A routine built only on retirement is a repair routine. The four earlier practices are what keep a hose out of the failure statistics in the first place. On our own test bench, hoses that are drained and warmed correctly show cover and coupling condition far closer to new after the same number of steam cycles than hoses run wet from cold.
Steam hoses and fittings are a system, and the maintenance routine has to treat them as one. A perfect hose with a corroded coupling is a leak waiting for a pressure cycle, and a perfect coupling on a hose stored in a coil on the floor is a kink waiting for a warm-up.
Tip 1: Store a Steam Hose So It Cannot Take a Set
A steam hose that lies in the same tight coil for months develops a memory. The tube takes a set (compression set), the reinforcement holds the curve, and the first time the hose is straightened under pressure the strain concentrates at the inside of the bend. Storage is therefore a maintenance action, not housekeeping.
Correct steam hose storage has four conditions:
- Support, do not stack. Hang the hose on a wide-radius rack or lay it in a straight run. Coil diameter should be generous — a tight coil is a permanent bend.
- Keep it out of sunlight and away from ozone sources. Ultraviolet light attacks the cover compound, and electric motors, welding sets and switchgear generate ozone that does the same.
- Keep it clean and dry inside. Residual condensate left in a stored hose keeps the tube wet for weeks and can leave mineral deposits that later flake into the steam path.
- Protect the ends. Cap or bag the couplings. Threads and gasket faces that pick up grit in storage become leak paths in service.
Table 1 sets out the storage conditions we check in our own hose store, with the condition a hose should be in when it is put away.
Table 1. Steam hose storage conditions by hose state, with the acceptance condition at put-away
| Hose state | Storage condition | Accept for storage |
|---|---|---|
| New, never used | Original coil or straight run, ends capped, flat rack, dark store | Cover intact, no set, coupling caps in place |
| In rotation, dry | Wide-radius rack, drained, ends bagged | No visible condensate when the end is lowered |
| In rotation, wet | Drain first, then rack; never store a wet hose coiled | Bore clear, no water trapped in a low loop |
| Awaiting decision | Segregated area, tagged with the finding and the date | Tag legible; hose not returned to the rack |
Storage discipline pays off at the next start-up. A hose that comes off the rack straight and dry heats evenly along its length. A hose that comes off the floor still wet in a tight coil heats unevenly, and the condensate it traps will arrive at the coupling as a slug rather than as a flow.
It is also worth recording where the hose was stored. A plant that tracks a steam hose replacement back to a storage position frequently finds that the same rack, the same wall or the same corner keeps producing early failures, while the hose itself was never the problem.

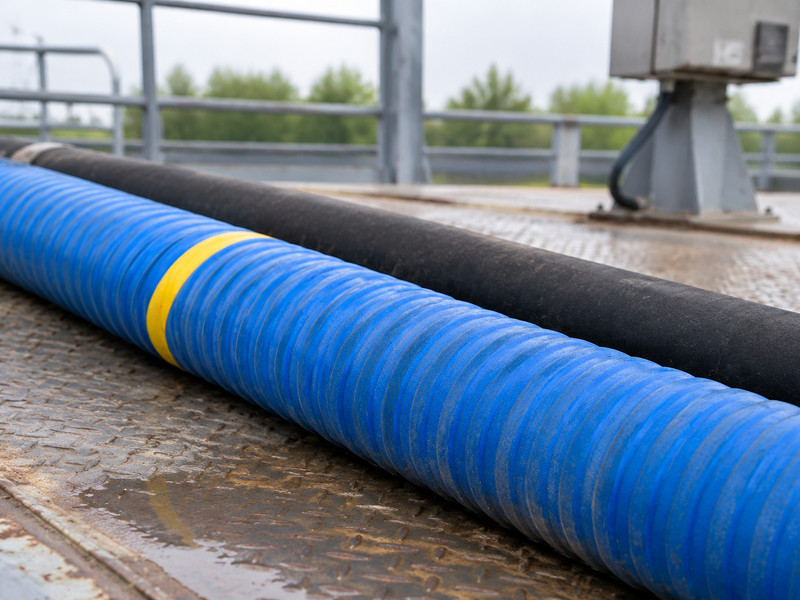
Figure 2. Storage that meets the rule: wide radius, off the floor, ends capped, and an identification tag that records when the hose was last inspected.
Tip 2: Run a Two-Minute Check Before Every Shift
The pre-shift check is the highest-value two minutes in steam hose maintenance, because almost every steam hose failure announces itself before it happens. The trick is to look for the four things that actually predict failure, rather than to give the hose a general once-over.
Check these four, in this order:
- The cover, along its whole length. Look for blisters and soft bulges, which mean steam is collecting between the tube and the cover instead of venting through the perforations.
- The couplings and the ferrule or clamp. Look for weeping at the joint, movement between the hose and the fitting, and any sign the coupling has been dragged or dropped.
- The outside of the hose at the bend points. Look for cracking, hardening and flattened sections. Hardening means heat aging; flattening means a kink that has already damaged the reinforcement.
- The restraint, where one is fitted. Check that it is attached at both ends and seated so it cannot chafe the cover during a pressure cycle.
Table 2 gives the acceptance criteria we use when training operators on a steam line. Anything in the reject column takes the hose out of service before the shift starts, not after the first incident.
Table 2. Pre-shift acceptance criteria for a flex hose for steam duty
| Überprüfen | Accept | Reject and tag out |
|---|---|---|
| Cover condition | Uniform, perforations clear, dry to the touch | Blister, bulge, cut to the reinforcement, soft spot |
| Coupling joint | No weeping, no relative movement, markings legible | Any leak at the joint, movement, or missing marking |
| Straightness under hand pressure | Returns to a straight run, no flat section | Persistent kink or flattened wall |
| Cover hardness at the bend | Flexible, similar along the length | Hard or brittle section next to a flexible one |
| Restraint | Attached both ends, seated, not chafing | Missing, slack, or cutting into the cover |
The check takes two minutes once it is a habit, and it produces a decision, not an impression. That matters for a flex hose for steam because the failure mode is not gradual: a blistered cover can hold for weeks and then split on the next warm-up. The pre-shift check follows the practice set out in ARPM IP-11-1.
Tip 3: Control the Warm-Up, Because Steam Admission Is the Destructive Step
The most damaging minute in a steam hose’s working day is the minute it first sees steam. A hose that has been standing cold at ambient temperature becomes a heat exchanger the instant the valve opens: steam condenses against the cold tube wall, the condensate runs downhill, and the slug of water it forms accelerates until it hits a bend or a coupling. That is water hammer, and on a steam line it is a condensate event rather than a pressure surge.
A controlled warm-up avoids it. Saturated steam temperature is fixed by the pressure: about 165 °C at 6 bar (gauge) and 210 °C at 18 bar, the top of the ISO 6134 Type 2 envelope. The sequence we recommend has five steps, and none of them is optional on a high pressure steam hose:
- Open the drain first. Condensate has to leave the line before steam follows it. Admit steam only after the drain is open and flowing.
- Crack the valve, do not open it. A small opening warms the tube gradually and lets the line drain as it heats.
- Watch the drain, not the gauge. When the drain runs dry steam rather than water, the line is warm and the hammer risk has passed.
- Bring the hose up to full pressure in stages. Each stage lets the tube and the reinforcement catch up with the temperature change together.
- Re-check the couplings once hot. Thermal expansion is the moment a marginal joint starts to weep, and it is far safer to find it during a controlled warm-up than later.
Table 3. Warm-up sequence for a steam hose, with the purpose and the observation that ends each step
| Step | Purpose | Observation that ends the step |
|---|---|---|
| 1. Open the drain | Remove standing condensate before steam arrives | Drain flowing freely, no water pooling at the low point |
| 2. Crack the valve | Warm the tube gradually instead of shocking it | Line beginning to warm along its length |
| 3. Hold at low flow | Let condensate leave as fast as it forms | Drain running dry steam, not wet |
| 4. Raise pressure in stages | Let tube and reinforcement expand together | Pressure steady at each stage before the next |
| 5. Re-check when hot | Catch joint weeping caused by thermal expansion | Couplings dry, no movement, restraint seated |
Warm-up is also where the rating discipline from why EPDM is the standard for saturated steam has to meet the gauge. A hose rated at a working pressure still fails while the gauge reads a working pressure if steam is admitted as a slug instead of a flow. A slug reaching a bend presents a local pressure well above the gauge reading. The relationship between the rating and the pressure that bursts a hose is set out in our note on working pressure and burst pressure.
Tip 4: Drain Condensate Before and After Every Use
Condensate is the reason a steam hose fails from the inside out. At the same pressure it holds far more heat per unit volume than the steam beside it, it carries dissolved solids, and it sits in the low points of a hose that is not drained. Two drainages, at the start and at the end of every use, remove most of that exposure.
Drainage practice that works on the floor looks like this:
- Drain the line, not just the hose. A closed drain upstream simply refills the hose from the header the moment the hose drain is closed.
- Drain from the lowest point. On a run with a sag, that may not be the hose end; support the run so it falls to one drain.
- Blow the hose clear, then leave the ends open. A hose stored with the ends open dries; a hose stored with the ends closed stays wet.
- Check the steam trap as part of the routine. A failed trap is a condensate generator, and it will undo every drainage habit on the line.
Drainage is also where bore size stops being a purchasing decision and becomes a maintenance one. A hose with a small bore drains slowly and traps more water at a given slope, while an oversized bore on a short run holds a larger volume of condensate whenever the line shuts down. Our hose size selection note covers how the two are balanced at specification stage; here the point is simpler, that a hose that cannot drain cannot be maintained.

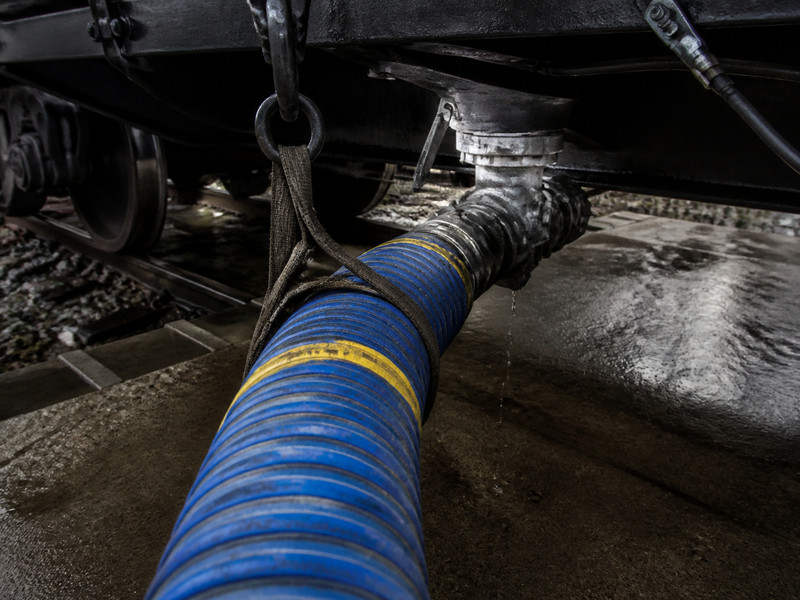
Figure 3. Drainage at shutdown: condensate leaves from the lowest point of the run, and the trap station is checked in the same pass.
Tip 5: Retire on Evidence: When Steam Hose Maintenance Becomes a Replacement Decision
Every steam hose reaches a point where further maintenance is wasted effort. The task is to recognize that point from evidence rather than wait for a leak, because the failure that ends a neglected hose’s life is rarely the cheap one.
Use the four signals below as retirement triggers. Any one of them is enough; two together make the decision easy.
- A cover defect that reaches the reinforcement — a cut, gouge or split that exposes the wire or textile layer. The reinforcement is the pressure-retaining element, and once it is exposed its condition can no longer be judged from the outside.
- A bulge, blister or soft spot that survives a pressure cycle. This is a separation between tube, reinforcement and cover, and it progresses.
- Hardening along part of the length with cracking at the bend points. Heat aging is cumulative and does not reverse.
- A repaired leak that has moved. A hose repaired successfully once and leaking again at a different place has told you the tube is at the end of its life, not that the repair failed.
Table 4. Steam hose replacement decision matrix used in our maintenance reviews
| Finding | Immediate action | Replacement decision |
|---|---|---|
| Cover cut to the reinforcement | Remove from service, tag out | Replace; no repair |
| Persistent blister or soft spot | Remove from service | Replace; record the position and the service hours |
| Localized hardening with cracking | Remove from service now | Replace at the next planned window |
| Weeping at the coupling, hose sound | Isolate, re-make the joint to specification | Keep if the assembly passes its check when hot |
| Second leak at a new position | Remove from service | Replace, and review the service conditions |
| No defect but the record is missing | Inspect fully and re-tag | Decide on the re-inspection result, not on age alone |
Two habits make the retirement decision reliable. The first is a tag that travels with the hose and records the last inspection, so the decision starts from facts. The second is a full inspection at the tag date, using the same criteria your crew uses in the pre-shift check. The hose inspection checklist we publish covers the same ground for industrial hose generally, and a steam hose fails in the same four ways. A steam hose replacement driven by a tag date costs a hose; a steam hose replacement driven by a burst costs a shutdown.
The Steam Hose Maintenance Schedule: Daily, Monthly and Annual Work
Five practices become manageable once they are attached to a clock. Table 5 is the schedule we hand to a plant that is setting up a first routine. It assumes one shift-based crew and a maintenance technician who owns the records.
Table 5. Steam hose maintenance schedule, with the record each task produces
| Interval | Task | Record produced |
|---|---|---|
| Every shift | Pre-shift check of cover, couplings, bend points and restraint | Tag initialled, or a defect raised |
| Every use | Warm-up sequence and shutdown drainage | Drain check noted on the run sheet |
| Monthly | Storage area check, hose rotation, trap condition review | Storage and trap findings log |
| At the tag date | Full inspection against the retirement criteria | Inspection record and keep or replace decision |
| Annually | Review of replacement rate, repeat failure positions and service conditions | Updated spare-holding and specification review |
The annual review is the step that most plants skip, and it is the one that changes the replacement rate. If the same hose position appears twice in a year’s replacement list, the hose is not the problem. The position is, and the fixes are usually cheap: an extra support, a wider bend radius, a drip leg, a smaller bore that drains properly. Record keeping at this level is also how you replace guesswork with a service-life figure you can defend, as set out in our service-life planning for industrial hose.
What Steam Hose Maintenance Cannot Fix
A maintenance routine protects a hose that was specified correctly. It cannot rescue one that was not, and four specification errors account for most of the hoses that keep coming back to the store.
- A working pressure chosen at the maximum. A hose run continuously at its rated pressure has no margin for a warm-up stage or a pressure fluctuation. Choose the class with room above the line pressure.
- A bend radius tighter than the hose allows. No amount of inspection prevents a kink; only a longer hose, a support or a wider radius will.
- A bore that holds condensate. Drainage cannot empty a hose that sags below its own drain point.
- A duty above the hose’s temperature envelope. Saturated steam at a given pressure has one temperature, and running above the envelope ages the tube faster than any other single factor.
The same four errors drive most early replacements on a high pressure steam hose line, and they are all cheap to correct at the specification stage and expensive to correct at the maintenance stage.

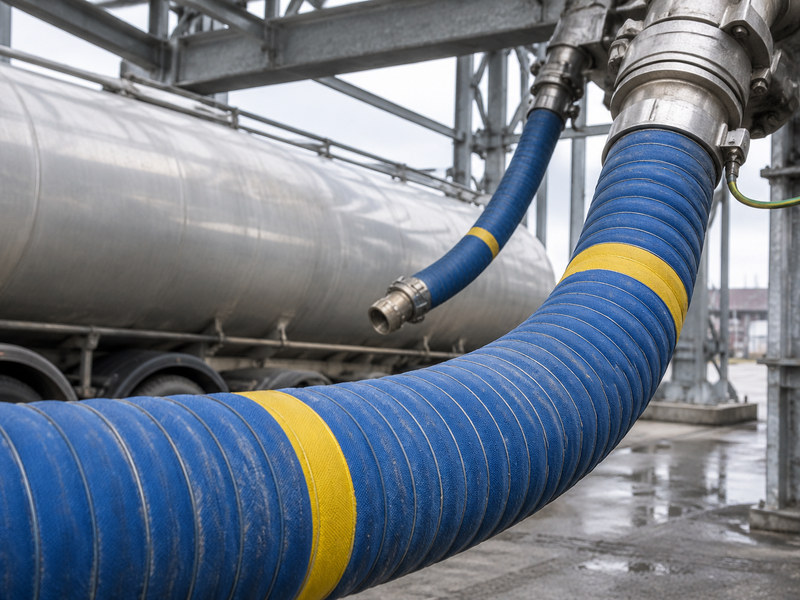
Figure 4. Specifying for maintenance: a supported run, a bend radius the hose can accept, and a drip leg that gives condensate somewhere to go.
When a hose position keeps consuming hoses, the right response is a program rather than another routine. That is the step described in our note on why a steam hose inspection program matters, which is the same five practices here, given a frequency policy and a record that outlives the crew that wrote it.
Steam Hose Maintenance FAQs
How often should the crew check a steam hose on shift?
A visual and hand check before every shift, and a full inspection at the date on the hose tag. The pre-shift check finds cover damage, coupling weeping and restraint faults in about two minutes. The full inspection applies the retirement criteria and produces a written keep-or-replace decision. Hoses in continuous service should be tagged with an inspection date that reflects the duty and the site’s own experience, not a single interval copied from another plant.
Can a steam hose be repaired?
A leaking coupling joint can usually be re-made to specification if the hose itself is sound. A defect that reaches the reinforcement cannot be repaired; a cover cut, gouge or split that exposes the wire or textile layer compromises the pressure-retaining element, and a patch only hides it. Blisters, soft spots and localized hardening are also replacement findings rather than repair findings, because they show that the tube, reinforcement and cover have already separated.
Why does my steam hose blister?
Blisters appear when steam permeates through the tube and collects between the tube and the cover instead of venting. The cover on a steam hose is perforated for exactly that reason, so blistering usually means the perforations are blocked, the cover has been painted or taped over, or the hose is running hotter than its envelope allows. Check the cover treatment and the duty temperature before assuming the hose is at fault.
What does a leak at the coupling mean?
A wet joint is a joint problem first and a hose problem second. Thermal expansion during warm-up is when marginal joints start to weep, which is why re-checking the couplings once the hose is hot finds so many of them early. Re-make the joint to specification and check the gasket face for grit or scoring. If weeping returns after a correct re-make, the hose end is suspect and the assembly should be inspected fully.
Where should a steam hose go when a shift ends?
Drained, supported and capped. Lay the hose in a wide-radius rack or a straight run rather than a tight coil, keep it out of direct sunlight and away from motors and welding equipment, and leave the ends open so the bore dries. Cap or bag the couplings so grit cannot reach the threads or the gasket faces. Proper steam hose storage prevents the set, the kink and the deposits that appear later as failures in service.
Does a high pressure steam hose need a different routine?
It needs the same five practices with tighter tolerances. A high pressure steam hose is usually wire reinforced, so it is heavier and harder to support, its warm-up needs more stages, and a failure releases more stored energy. That increases the value of the pre-shift check on the couplings and the restraint. The practices themselves do not change; what changes is how much margin you keep above the line pressure.
What causes water hammer in a steam hose line?
Condensate meeting a flow of steam. Steam condenses against a cold tube wall, the water collects at a low point, and the moving steam accelerates the slug until it strikes a bend or a coupling. It is a drainage and warm-up problem, not a pressure problem. The cure is the same in every plant: open the drain first, warm the line gradually through a cracked valve, and raise pressure in stages.
Should a steam hose be replaced on a date or on evidence?
Service life should be judged on evidence rather than on a date. It depends on duty temperature, pressure cycles, condensate quality, how often the hose is moved, and whether the run drains properly. A defensible answer comes from the plant’s own replacement records once they cover a few years of the same position. Until then, retire a hose when the inspection criteria say so, not when a calendar says so.
Which steam hoses and fittings need a restraint?
Any assembly whose disconnection could injure someone or damage equipment, which in practice means any pressurized steam line above a small bore. A restraint is a retention device at the coupling; it limits travel if the connection fails, and it must be fitted so it cannot chafe the cover under pressure. Steam hoses and fittings on a coupling that can move, or on a hose that can whip, are the cases worth fitting first.
How do I choose a flex hose for steam duty?
Start from the saturation temperature at the line pressure, because saturated steam pressure and temperature are one variable. Then choose the pressure class with margin above the line pressure, a cover that resists the oils and chemicals around the plant, and a bore that drains at the slope available. A flex hose for steam also has to be long enough to accept the bend radius it will see. Match the end connections at the same time, not afterwards.
Final Verdict: Five Steam Hose Maintenance Habits Worth Keeping
Steam hose maintenance is not a specialist job, and it does not need new equipment. It needs five habits, attached to a clock, and one record.
- Store it straight, dry, dark and capped so the hose starts the next job with no set and no deposits.
- Spend two minutes before every shift on the cover, the couplings, the bend points and the restraint.
- Open the drain and crack the valve before admitting steam; the warm-up minute is the one that damages hoses.
- Drain at both ends of every use, and treat a failed steam trap as a maintenance finding, not a nuisance.
- Retire on the four evidence signals and review the year’s replacements to find the positions that keep consuming hose.
HENGHUA manufactures steam hose range — steam hose assemblies, industrial hose couplings and end connections — for distributors, EPC contractors and OEM brands. The steam hose range is built on an EPDM tube with textile or steel-wire reinforcement and a perforated, oil-resistant cover, in bore sizes and pressure classes covering both ISO 6134 type envelopes. The catalog also carries a high-temperature grade for duties above the saturated-steam range.
Assemblies are terminated with bolted safety clamps, crimped or swaged ferrules, flanged ends and cam and groove couplings, in carbon steel, 304/316 stainless steel and brass. Every assembly is tested to its rated working pressure before shipment and marked with its size, working pressure and identification code.
Factory-direct pricing, short lead times on bulk orders, private labeling and OEM branding are all standard. For a quotation, sample or help setting up a maintenance routine for your own steam lines, contact our engineering team.
About the author. Written by the HENGHUA engineering team, which designs and pressure-tests steam hose and industrial hose assemblies and supports distributors and plant maintenance departments with hose selection, installation and inspection practice. The team’s guidance is drawn from assembly and test records on the steam hose line and from field reviews with customers in tire, precast concrete, chemical and general manufacturing plants.


 English
 Spanish
 Portuguese
 French
 German
 Arabic
 Russian
 Indonesian
 Japanese
 Korean