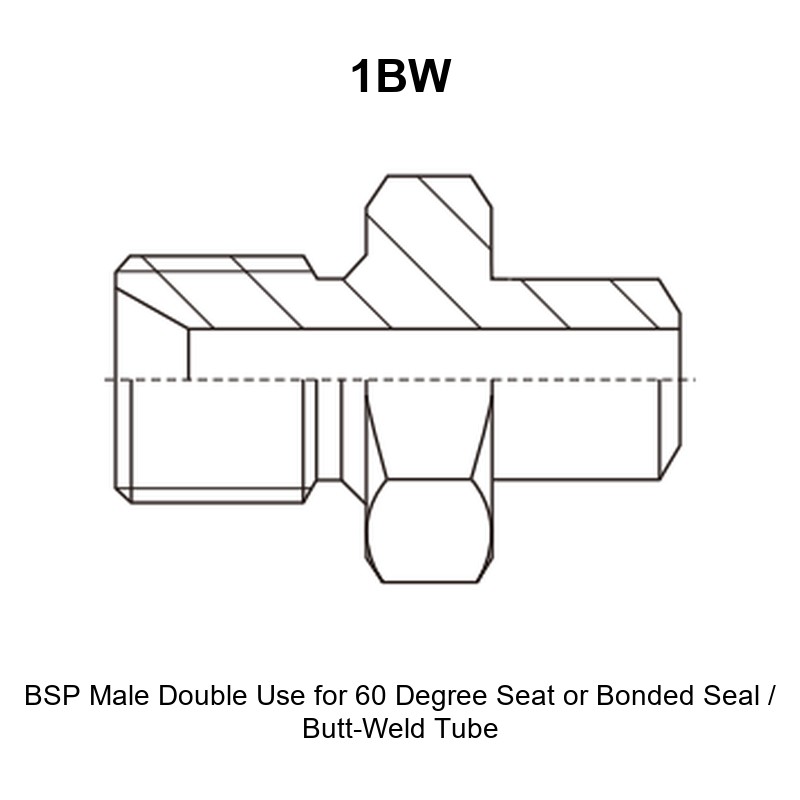
The 1BW adapter is a straight hydraulic fitting that joins a BSPP (G thread) port to a tube that is butt-welded to the adapter. Connection 1 is a BSP male stud built for double use: it seals on an ISO 1179 60° cone seat or on a bonded seal against a flat face. Connection 2 is a weld end that carries no thread and no seal element; the joint is closed by welding the adapter to the tube. HENGHUA machines the thread to the published port standard and the weld end to the tube size, so each end matches what it is joined to, which is the precondition for eliminating leakage at the connection point.
1. What a 1BW Adapter Does
A 1BW adapter connects a BSPP (G) threaded port to a tube line, or a tube line to a BSPP port, at a fixed angle on the tube axis. It is a rigid straight body, and unlike an all-threaded adapter it uses one welded joint instead of a second threaded joint, which removes a potential leak path at the tube side.
The two ends are of different kinds. The BSPP end is a threaded stud that is double use: it seats metal to metal on a 60° cone where the port has a cone, or compresses a bonded washer (Dowty-type) against a flat face. The tube end is a weld preparation, welded to the tube outside diameter listed for that part number, so the joint is a welded connection in the tube run rather than a sealed threaded connection.
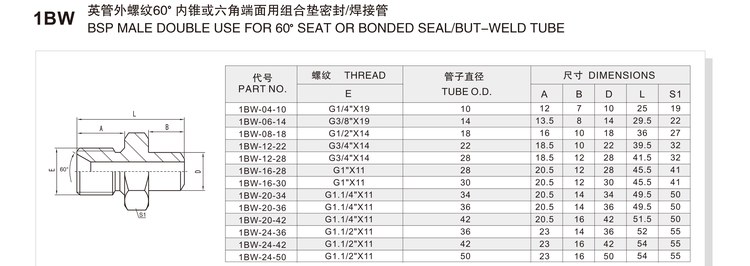
Because the weld end is matched to a tube size, the part number fixes both ends at once: a thread size on the BSPP side and a tube outside diameter on the weld side. The catalogued range covers BSPP sizes from G1/4″X19 to G1.1/2″X11 and tube outside diameters from 10 mm to 50 mm, and the chart lists the stud length, the weld-end length, the tube dimension, the overall length and the hex for each pairing. Supplied as a BSP adapter at the port end, it is ordered as a bonded seal adapter when the BSPP port is flat-faced. Compared with a hose adapter fitting, the weld end removes one threaded joint from the line.
2. 1BW Adapter Specifications
The specification is presented as two mirrored ends, so a buyer can read off which end goes to which connection before ordering.
2.1 Connection 1 – BSPP male, 60° cone seat or bonded seal
| Artículo | Specification |
|---|---|
| Thread standard | ISO 228-1 (BSPP / G thread), port geometry per ISO 1179 |
| Thread family | Parallel BSP pipe thread, G series, 55° thread form |
| Sizes available | G1/4″X19 to G1.1/2″X11 |
| Gender | Male stud end |
| Sealing method | Double use: 60° cone seat against a mating cone, or bonded seal on a flat face |
| Mating port | ISO 1179 BSPP port with 60° cone seat, or ISO 1179 flat-faced BSPP port with bonded seal |
2.2 Connection 2 – Butt-weld tube end
| Artículo | Specification |
|---|---|
| Joint type | Butt weld between the adapter weld end and the tube, no thread and no seal element |
| Tube outside diameter | 10 mm to 50 mm, per the TUBE O.D. and D columns of the table below |
| Gender | Neither; the end is a weld preparation sized to the tube |
| Sealing method | Full-penetration weld around the tube circumference; pressure tightness is made by the weld |
| Mating part | Steel tube or pipe of the listed outside diameter and a suitable wall thickness for the system pressure |
Note on the weld end: the weld end is not a threaded port and takes no bonded washer or O-ring. Its dimensions are matched to the tube outside diameter in the chart, and the tube wall thickness is chosen by the system working pressure, so the wall thickness is specified by the buyer or confirmed with HENGHUA engineering for critical circuits. The BSPP end follows ISO 1179, and its 60° cone option corresponds to the cone stud end family covered by ISO 8434-6.
2.3 Construction and Materials
| Artículo | Options |
|---|---|
| Body material | Carbon steel; 304 stainless steel; 316 stainless steel; brass |
| Plating | Trivalent chromium zinc plating (Cr3+); zinc-nickel plating |
| Seal material | NBR, FKM (Viton-type), EPDM for the bonded seal option at the BSPP end |
| Form | Straight, one-piece, machined from bar stock, with a weld preparation turned at the tube end |
| Machining | CNC turning with the BSPP thread cut to the port standard and the weld end turned concentric to the thread; thread gauges and dimensional checks applied batch by batch before packing |
| Wrenching | Hex flats on the body, sized per the S1 column, for holding the part during installation and during welding |
2.4 Pressure and Temperature
Working pressure for this series is governed by the size, the body wall thickness, the tube wall thickness used at the weld, the sealing method used at the BSPP end and the material selected, and it is confirmed per order by HENGHUA engineering against the drawing. No single pressure figure applies to the whole series, because the welded joint and the tube carry the load together; the rating is quoted with the quotation for the specific part number and material.
Seal material temperature ranges are material facts rather than ratings of the assembly: NBR approximately -30°C to +100°C; FKM (Viton-type) approximately -20°C to +200°C; EPDM approximately -40°C to +120°C. Carbon steel with zinc plating suits general hydraulic service; 304 and 316 stainless steel are specified for corrosive and offshore environments. Where the tube end is to be welded, the welding procedure and any post-weld treatment belong to the fabricator and must respect the material selected for the body.
2.5 Part Number and Dimension Table
Column meanings: PART NO. is the ordering code; THREAD E is the BSPP (G) stud end; TUBE O.D. is the tube outside diameter in mm that the weld end joins; A is the length of the BSPP stud end in mm; B is the length of the weld end in mm; D is the tube dimension printed at the weld end in mm, which repeats the tube outside diameter in every row of the chart; L is the overall length in mm; S1 is the hex across flats in mm.
| PART NO. | THREAD E | TUBE O.D. | A | B | D | L | S1 |
|---|---|---|---|---|---|---|---|
| 1BW-04-10 | G1/4″X19 | 10 | 12 | 7 | 10 | 25 | 19 |
| 1BW-06-14 | G3/8″X19 | 14 | 13.5 | 8 | 14 | 29.5 | 22 |
| 1BW-08-18 | G1/2″X14 | 18 | 16 | 10 | 18 | 36 | 27 |
| 1BW-12-22 | G3/4″X14 | 22 | 18.5 | 10 | 22 | 39.5 | 32 |
| 1BW-12-28 | G3/4″X14 | 28 | 18.5 | 12 | 28 | 41.5 | 32 |
| 1BW-16-28 | G1″X11 | 28 | 20.5 | 12 | 28 | 45.5 | 41 |
| 1BW-16-30 | G1″X11 | 30 | 20.5 | 12 | 30 | 45.5 | 41 |
| 1BW-20-34 | G1.1/4″X11 | 34 | 20.5 | 14 | 34 | 49.5 | 50 |
| 1BW-20-36 | G1.1/4″X11 | 36 | 20.5 | 14 | 36 | 49.5 | 50 |
| 1BW-20-42 | G1.1/4″X11 | 42 | 20.5 | 16 | 42 | 51.5 | 50 |
| 1BW-24-36 | G1.1/2″X11 | 36 | 23 | 14 | 36 | 52 | 55 |
| 1BW-24-42 | G1.1/2″X11 | 42 | 23 | 16 | 42 | 54 | 55 |
| 1BW-24-50 | G1.1/2″X11 | 50 | 23 | 16 | 50 | 54 | 55 |
Table note: every row of the current chart for this series is reproduced above. The chart as supplied covers tube outside diameters from 10 mm to 50 mm; other tube sizes are quoted on request: [VERIFY WITH SUPPLIER]. All dimensions are in mm and are confirmed against the drawing for the exact part number at order stage, including the weld preparation details for the tube wall thickness you intend to use.
3. How to Read a 1BW Adapter Part Number
The code has three blocks. 1BW is the series: BSP male double use for 60° seat or bonded seal, with a butt-weld tube end. The first number after the prefix is the BSPP (G) size, counted in sixteenths of an inch. The second number is the tube outside diameter in mm, not a thread size.
Worked example: 1BW-12-28 decodes as 1BW series, 12 = 12/16 in = G3/4″X14 on the BSPP side, 28 = 28 mm tube outside diameter at the weld end. The chart gives A = 18.5 mm, B = 12 mm, D = 28 mm, L = 41.5 mm and hex S1 = 32 mm.
Size code reference from the table above: BSPP side 04 = G1/4″X19, 06 = G3/8″X19, 08 = G1/2″X14, 12 = G3/4″X14, 16 = G1″X11, 20 = G1.1/4″X11, 24 = G1.1/2″X11. Tube side 10, 14, 18, 22, 28, 30, 34, 36, 42 and 50 are tube outside diameters in mm. The same tube diameter appears against more than one BSPP size, for example 28 mm against both G3/4″X14 and G1″X11, so the tube size alone does not identify the part.
4. Installation and Fitment
Preparation decides the result at both ends. At the BSPP end, clean the port, remove old sealant residue, and confirm that the port face is unmarked if a bonded washer is to be used, because a washer cannot bridge a scored or dented face. At the tube end, cut the tube square, deburr inside and outside, and check that the tube outside diameter matches the TUBE O.D. column of the part number before welding.
Welding. Tack the adapter to the tube with the body held on its hex so the thread is not heated unnecessarily, check the alignment of the BSPP end against the port it will enter, then complete the weld around the circumference with a procedure suited to the body material and the tube material. Cool the part in air and clean the weld before assembly, so no scale reaches the cone seat or the bonded washer face. Where the tube and the adapter are of different materials, the welding procedure must be chosen for that combination.
Assembly at the port. Fit a bonded washer where the BSPP port is flat-faced, or locate the 60° cone where the port has a cone, run the stud in by hand and then tighten it snugly while holding the body on the hex. Never use the hex to jack the other end of a welded assembly into position, because the tube run cannot absorb the load. Tightening torque and angle are confirmed per order and per size by HENGHUA engineering.
Reuse and common errors. The welded joint is permanent; the BSPP joint is not, and the bonded washer is a single-use item that is replaced whenever that joint is broken. Common fitment errors and symptoms: a tube end cut out of square shows as a weld that is thin on one side and a joint that weeps at the weld; a tube of the wrong outside diameter will not seat on the weld preparation and produces a step inside the bore; a re-used washer shows as weeping at the hex shoulder; and a BSPT male end turned into a BSPP port damages both threads, because a taper thread and a parallel thread are not interchangeable.
5. Applications and Industries
Application tags: hydraulic systems, water jetting, oil and gas, industrial equipment, construction machinery, agriculture, marine, material handling.
Cross-standard equipment integration. Where a machine carries BSPP ports and the line is built from tube rather than hose, this series makes the transition from a tube run to the port with one welded joint and one threaded joint, instead of two threaded joints.
Repair and replacement. Maintenance teams keep the series for tube repairs on mixed-standard machinery, because the weld end can be cut off and re-welded while the BSPP end remains the interface to the existing port.
High-pressure test benches. Test circuits are often built from tube for stiffness, and the weld end removes a threaded joint from the pressure line, which simplifies leak tracing on the panel.
OEM assembly lines. For a new build the series can be supplied to a drawing with a fixed plating, bonded seal choice and weld preparation, so the line receives one part number per tube-to-port junction and a repeatable weld geometry.
6. Replacement and Cross-Reference Guide
Cross-reference this series by standard, thread, tube size and sealing method only, never by another maker’s catalogue number. Identify the port type, the tube size and the seal at the BSPP end, then match the row.
Measure these three things. First, the thread: measure the outside diameter of the BSPP stud, count the threads per inch and match the G column, such as G3/4″X14. Second, the tube: measure the tube outside diameter with a caliper and match it to the TUBE O.D. column, and measure the tube wall thickness, because the wall carries part of the working pressure. Third, the seal: look inside the BSPP port. A 60° cone means the stud seals on the cone; a flat face means it seals on a bonded washer.
Replacement rules. A welded adapter is replaced by the same series and the same row when the tube size and the BSPP thread both match; if the existing tube is a different outside diameter, select the row for that tube and confirm the weld preparation against the drawing. If the port is a BSPT taper thread, this series is not the equivalent, because the 1BW BSP end is a parallel G thread. Where the whole tube run is to be re-made rather than re-welded, a threaded alternative such as a BSP male to BSP female adapter can be considered instead.
7. Ordering, Packaging and Delivery
To order, give the series code plus the full part number, the BSPP thread size, the tube outside diameter and wall thickness, the seal material, the plating and the quantity, for example: 1BW series, 1BW-12-28, G3/4″X14 to 28 mm tube O.D. with 3 mm wall, FKM bonded seal, trivalent chromium zinc plating on carbon steel, 300 pieces. If the port is a 60° cone port, say so and the bonded washer is dropped from the quote.
Packaging. Parts are packed in cartons with the part number and quantity labelled, in bulk or in poly bags as the order requires, and can be labelled for distributor shelves or for direct-to-line OEM delivery. Weld ends can be supplied with protective caps so the weld preparation arrives clean, and mixed-size cartons are labelled line by line.
Samples and lead time. Sample quantities are available for validation before a production order, including with the nominated bonded seal material and plating, so the weld preparation and the port joint can both be checked, and lead time is confirmable per order and per size once the specification is fixed.
8. FAQ
What is the difference between BSPP and BSPT, and can they be interchanged? BSPP (G thread, ISO 228-1) is a parallel thread where pressure tightness is not made on the threads, so the joint seals on a 60° cone seat or on a bonded washer against a flat face. BSPT (R, Rc, Rp thread, ISO 7-1) is a taper thread where pressure tightness is made on the threads and a sealant is required. They are not interchangeable: forcing a taper male into a parallel female port damages both threads and will not seal reliably.
What is the difference between a 60° cone seat and a bonded seal, and which should I choose? The 60° cone seat seals metal to metal where the male cone meets the matching cone in the port and needs no extra sealing element. A bonded seal (Dowty-type washer) seals on a flat face and is compressed between the hex shoulder and the port face. Choose by the BSPP port you have: a cone calls for the cone seat, a flat face calls for the bonded washer. The tube end of this series needs neither, because it is welded.
How do I identify the correct 1BW size? Read the port and the tube, not the old part alone. Measure the BSPP thread and match it to the G column, then measure the tube outside diameter and match it to the TUBE O.D. column, and pick the row where the two meet. Because one tube diameter is listed against more than one BSPP size, both dimensions must be checked before ordering.
What seal material should I select for my fluid and temperature? NBR covers general hydraulic oil service at approximately -30°C to +100°C. FKM (Viton-type) suits higher temperatures and many aggressive fluids at approximately -20°C to +200°C. EPDM suits water-based fluids and steam at approximately -40°C to +120°C and is not compatible with mineral oil. The seal material applies to the bonded seal at the BSPP end; the welded tube end has no seal element.
How is the working pressure of this adapter determined? Pressure is not fixed across the series: it follows the size, the body wall thickness, the tube wall thickness at the welded joint, the sealing method at the BSPP end and the material, and it is confirmed per order by HENGHUA engineering with the quotation. The tube and the weld are part of the pressure boundary, so state the tube size, the wall thickness and the system working pressure on the inquiry.
What is the minimum order quantity and can I get samples? Sample quantities can be supplied for validation, including with a nominated bonded seal material and plating, so the weld end and the port joint can be checked before a production commitment. Minimum order quantity is confirmed per order because it depends on the size mix and the material. Send the part numbers with the annual quantity and both figures come back with the quotation.
Can the weld end be machined for a different tube wall thickness? Yes. The weld preparation is turned, so it can be produced for the tube wall thickness you weld to, provided the tube outside diameter matches the part number row. Send the tube specification and the drawing with the inquiry and HENGHUA confirms the weld preparation before the order.
Is the weld end suitable for stainless tube? The series is available in carbon steel with trivalent chromium zinc plating and in 304 or 316 stainless steel, so a stainless body can be welded to stainless tube with a procedure suited to that grade. Tell us the tube grade on the inquiry so the body material and the weld preparation are matched to it.
Browse the full Adaptadores hidráulicos range for the complete family, or contact us to request a quote, mill test reports, and samples.
 English
 Spanish
 Portuguese
 French
 German
 Arabic