Why This 90 degree elbow metric male o-ring butt weld tube adapter 1EW9 Passes the Compliance Gate
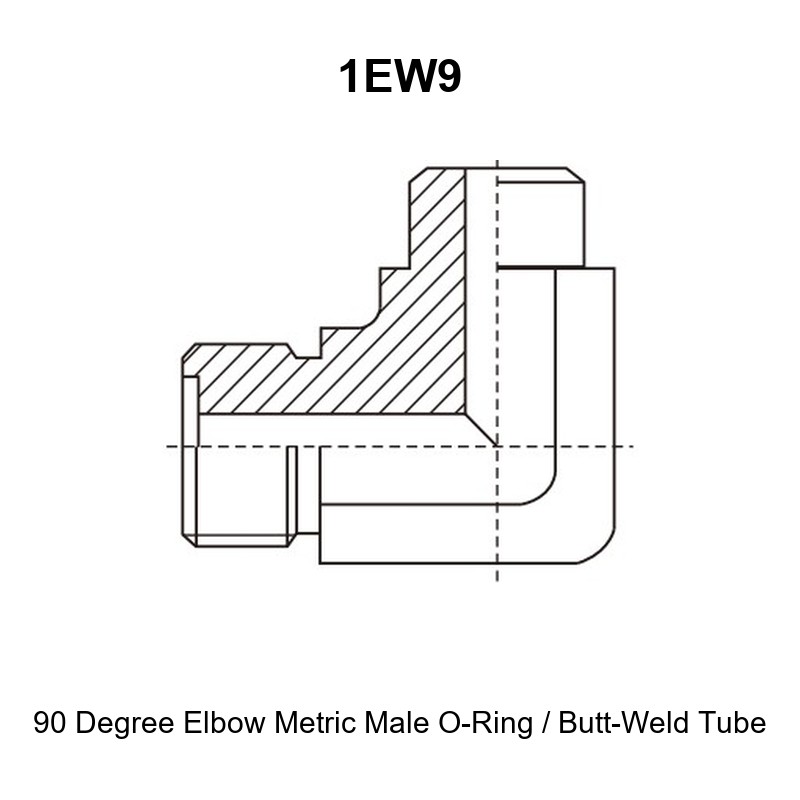
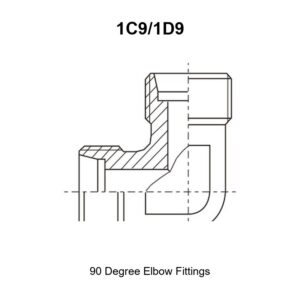
Connection 1 of the 90 degree elbow metric male o-ring butt weld tube adapter 1EW9 is a metric male stud end that seals with a captive O-ring on the flat face of an ISO 6149-2 / ISO 11926 port, from M12x1.25 to M52x2. Connection 2 is a plain butt-weld socket for tube from 6 mm to 42 mm outside diameter. The 90 degree body turns the circuit without a second fitting, and because the tube is welded rather than threaded, the run has no separable joint to loosen under vibration.
Buyers of this elbow are manifold builders, tube-race fabricators and maintenance engineers who must leave a machined block at a right angle. Welding the corner removes one threaded connection, one torque step and one stocked part number from every joint in the circuit.
Core Advantages
- Metric O-ring port compliance. The stud end threads into an ISO 6149-1 machined port and seals with the tabulated O-ring on the port face, with no thread sealant.
- Permanent butt-weld tube socket. Welding removes one threaded joint per corner, so there is nothing to re-torque after commissioning.
- Twelve tabulated sizes. M12x1.25 to M52x2 stud threads pair with 6 mm to 42 mm tube, each row carrying its own O-ring, L1, L2, D and S values.
- Right-angle layout in tight envelopes. The 90 degree form keeps the tube run parallel to the manifold face, which is often the only packaging option inside a machine frame.
- Documented, traceable supply. Batch traceability, dimensional records and material test reports support incoming inspection.
- OEM marking. Laser marking of your part number, logo and batch code is available, and finished elbows can ship as welded tube assemblies.
Technical Specifications
What Is a 90 degree elbow metric male o-ring butt weld tube adapter 1EW9?
It is a one-piece 90 degree adapter that joins an ISO 6149-2 metric male O-ring stud end to a weldable tube socket. The port seal is an elastomeric O-ring compressed on a flat machined port face, as defined for the metric O-ring stud end series.
It is not a DIN 2353 / ISO 8434-1 24 degree cone fitting, and it is not a 74 degree cone fitting from the SAE J514 family. A 24 degree or 74 degree stud seals on a cone inside the port, so the first checks are always the port standard, then the thread, then the tube.
Connection 1 – Metric male O-ring stud end (ISO 6149-2)
| Attribute | Especificações |
|---|---|
| Seal principle | Captive O-ring, face seal in an ISO 6149-1 machined port |
| Thread standard | ISO 6149-2 metric stud end (inch equivalents sit in the ISO 11926 family, a different series) |
| Threads in this series | M12x1.25, M14x1.5, M16x1.5, M18x1.5, M22x1.5, M27x1.5, M30x1.5, M36x2, M39x2, M42x2, M45x2, M52x2 |
| O-ring sizes in this series | 8×1.9, 10×1.9, 11×1.9, 13×1.9, 16×2.4, 20×2.4, 24×2.4, 30×3.1, 32×3.1, 35×3.1, 38×3.1, 40×3.1 |
| Stud hex across-flats (S) | 12 mm to 50 mm, per row of the matrix |
| Orientation | Fixed 90 degree body, no swivel |
Connection 2 – Butt-weld tube socket
| Attribute | Especificações |
|---|---|
| Weld end form | Plain socket, butt welded to tube |
| Tube outside diameter | 6 mm to 42 mm, twelve steps |
| Weld hub outside diameter (D) | Equal to the tube outside diameter in every row of this series |
| Weld preparation | Per the weld procedure agreed at order and general ISO 8434-1 / DIN 2353 practice |
| Tube wall thickness | [to be confirmed] against the qualified weld procedure for the application |
| Post-weld treatment | Clean, re-passivate or re-plate after welding where the weld procedure requires it |
Dimensional Data
| Symbol | Significado | Unit |
|---|---|---|
| E | Metric male stud thread at connection 1 | – |
| TUBE O.D. | Outside diameter of the tube butt welded into connection 2 | mm |
| O-RING (E end) | O-ring size designation at connection 1, written as inside diameter x cross-section | mm |
| L1 | Elbow reference dimension from the thread end to the centre line, as defined on the data-sheet drawing | mm |
| L2 | Second elbow reference dimension defined on the data-sheet drawing | mm |
| D | Weld hub / tube outside diameter | mm |
| S | Hex across-flats at the stud end (wrench size) | mm |
Full Dimension Table (Part Number Matrix)
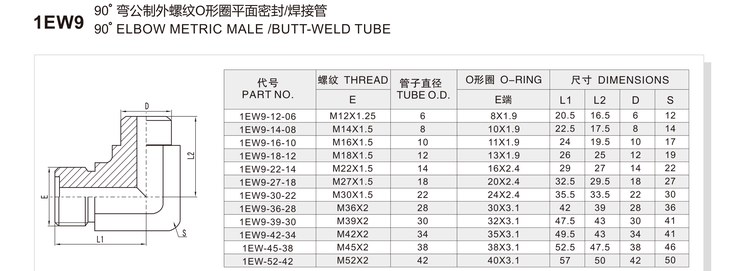
| PART NO. | THREAD E | TUBE O.D. | O-RING (E end) | L1 | L2 | D | S |
|---|---|---|---|---|---|---|---|
| 1EW9-12-06 | M12X1.25 | 6 | 8X1.9 | 20.5 | 16.5 | 6 | 12 |
| 1EW9-14-08 | M14X1.5 | 8 | 10X1.9 | 22.5 | 17.5 | 8 | 14 |
| 1EW9-16-10 | M16X1.5 | 10 | 11X1.9 | 24 | 19.5 | 10 | 17 |
| 1EW9-18-12 | M18X1.5 | 12 | 13X1.9 | 26 | 25 | 12 | 19 |
| 1EW9-22-14 | M22X1.5 | 14 | 16X2.4 | 29 | 27 | 14 | 22 |
| 1EW9-27-18 | M27X1.5 | 18 | 20X2.4 | 32.5 | 29.5 | 18 | 27 |
| 1EW9-30-22 | M30X1.5 | 22 | 24X2.4 | 35.5 | 33.5 | 22 | 30 |
| 1EW9-36-28 | M36X2 | 28 | 30X3.1 | 42 | 39 | 28 | 36 |
| 1EW9-39-30 | M39X2 | 30 | 32X3.1 | 47.5 | 43 | 30 | 41 |
| 1EW9-42-34 | M42X2 | 34 | 35X3.1 | 49.5 | 43 | 34 | 41 |
| 1EW-45-38 | M45X2 | 38 | 38X3.1 | 52.5 | 47.5 | 38 | 46 |
| 1EW-52-42 | M52X2 | 42 | 40X3.1 | 57 | 50 | 42 | 50 |
All dimensions are in millimetres and are transcribed row by row from the product data sheet. Thread codes are reproduced as printed, so M12X1.25 reads as M12x1.25 metric fine thread, and O-ring codes such as 16X2.4 read as 16 mm inside diameter by 2.4 mm cross-section. The two largest rows are printed as 1EW-45-38 and 1EW-52-42, without the trailing 9 in the prefix; they use the same 90 degree body and weld-socket geometry as the rest of the range.
Thread Size and Dash Chart
| Metric stud thread | Tube O.D. (mm) | Part number | O-ring at stud end | Hex S (mm) |
|---|---|---|---|---|
| M12x1.25 | 6 | 1EW9-12-06 | 8×1.9 | 12 |
| M14x1.5 | 8 | 1EW9-14-08 | 10×1.9 | 14 |
| M16x1.5 | 10 | 1EW9-16-10 | 11×1.9 | 17 |
| M18x1.5 | 12 | 1EW9-18-12 | 13×1.9 | 19 |
| M22x1.5 | 14 | 1EW9-22-14 | 16×2.4 | 22 |
| M27x1.5 | 18 | 1EW9-27-18 | 20×2.4 | 27 |
| M30x1.5 | 22 | 1EW9-30-22 | 24×2.4 | 30 |
| M36x2 | 28 | 1EW9-36-28 | 30×3.1 | 36 |
| M39x2 | 30 | 1EW9-39-30 | 32×3.1 | 41 |
| M42x2 | 34 | 1EW9-42-34 | 35×3.1 | 41 |
| M45x2 | 38 | 1EW-45-38 | 38×3.1 | 46 |
| M52x2 | 42 | 1EW-52-42 | 40×3.1 | 50 |
Material and Heat Treatment
| Item | Standard supply (typical) | On request |
|---|---|---|
| Body material | Carbon steel | Austenitic stainless steel for corrosive and offshore duty |
| Heat treatment | Stress relief applied as required by the drawing for carbon steel bodies | Grade and condition agreed per drawing |
| Surface treatment | Zinc-based plating | Zinc-nickel, chrome-free passivation, stainless passivation |
| O-ring elastomer | NBR, service range about -40 °C to +120 °C | FKM for higher temperature and aggressive media |
| Dimensional inspection | Sample and batch dimensional records | Full-lot dimensional report |
| Pressure testing | Batch pressure test with recorded results | Third-party witnessed testing |
| Documentation | Batch certificate and traceability record | Material test report on request |
The values above describe normal commercial practice for this family and are confirmed on the order drawing, not replaced by it.
Working Pressure and Operating Envelope
Because the data sheet for this series carries no pressure column, working pressure is governed by the port standard (ISO 6149-2 together with the ISO 6149-1 port) and by the tube wall and weld procedure selected, and the finished assembly is only as strong as its weakest member. The same elbow body ordered with different tube walls behaves differently, so no single headline figure is published for the family.
Ask for a rating table with your enquiry and we will state the figure and the test method for your thread size, tube wall, material and weld procedure. Where your specification calls for proof or burst testing of the finished assembly, that test is written into the order and the results travel with the shipment.
Temperature Range
The typical service window is -40 °C to +120 °C with a standard NBR O-ring, and the limit is set by the elastomer and the weld rather than by the steel body. FKM raises the upper limit for hot oil and some aggressive media. Confirm the elastomer for your fluid, and note that the welded joint sees the full circuit temperature with no separate seal to cushion it.
How to Read the Part Number Matrix
The order code carries three pieces of information: the elbow family prefix, the stud thread size, and the tube outside diameter.
- Prefix – 1EW9. The prefix states the end combination: metric male O-ring stud to butt-weld tube on a 90 degree body. Changing the prefix changes the ends, not the dimensions.
- Middle group – thread size. In 1EW9-22-14 the group 22 identifies the metric stud thread, M22x1.5.
- Final group – tube outside diameter. In the same code, 14 is the tube outside diameter in millimetres, which fixes the O-ring at 16×2.4, D at 14 and the hex at 22.
Two examples make the pattern clear. 1EW9-12-06 is the smallest row: M12x1.25 stud thread, 6 mm tube, 8×1.9 O-ring, hex 12. 1EW9-42-34 is a large manifold-row size: M42x2 stud thread, 34 mm tube, 35×3.1 O-ring, hex 41. For the two largest rows the data sheet prints the prefix as 1EW, so 1EW-52-42 is the M52x2 stud thread with 42 mm tube.
If you know only the thread or only the tube, quote that single value and we will return the matching row. For a worn part with no legible marking, send a photograph with caliper readings across the stud thread and across the weld hub.
Selection and Ordering
| Question | What to confirm before ordering |
|---|---|
| What port standard is on the manifold? | The port must be an ISO 6149-1 style flat-face O-ring port. A conical seat port takes a different stud family. |
| What is the stud thread? | Read the port callout, for example M22x1.5, and do not infer the thread from the port bore diameter. |
| What is the tube outside diameter? | Measure the tube and match a row, because the weld socket is sized to D. |
| What tube wall and weld procedure? | These drive the pressure capability of the finished joint, so state them at enquiry. |
| Is the O-ring material correct for the fluid? | NBR is the default; specify FKM or another elastomer for hot or aggressive service. |
| Will the hex clear? | The S value is the wrench size; check spanner and socket access before choosing a large row in a deep pocket. |
Cross Reference Service
Send an old part number, a photograph or a worn sample and we will cross it to the closest row of this matrix. The answer comes back with thread, tube size, O-ring and hex stated explicitly so you can verify it against your own measurement. The service is free, and we never re-label another maker’s part as our own or apply a third-party brand to our product.
Packaging and Logistics
Elbows ship in individual bags inside cartons, grouped by part number, with batch code and quantity on the outer label. Mixed cartons and mixed pallets are routine for distributors and repair workshops, and we consolidate several part numbers of this family into one shipment on request. Material test reports travel with the goods when ordered. Standard rows ship quickly from stock, and air freight covers urgent shutdown dates.
Installation and Fitment Guide
Step-by-Step Assembly
- Verify port standard, stud thread and tube size against this matrix before starting work.
- Check the port face for burrs, paint or old sealant, because an O-ring face seal needs a clean flat landing.
- Fit a new O-ring of the tabulated size, lightly lubricated with a compatible fluid, and check it sits fully in its groove.
- Thread the stud end in by hand until it seats, then tighten to the torque value for the thread size and material from the applicable standard data table.
- Cut and prepare the tube to drawing, set it squarely in the weld socket, and weld to the qualified procedure with the stud end shielded from heat.
- Let the joint cool, clean and treat the weld, then pressure test the finished assembly and record the result.
Torque and Sealing Notes
Tighten metric O-ring stud ends to the torque values for the thread size, material and coating from the applicable standard data table, and treat those figures as a starting point to be confirmed against your own test. An O-ring face seal does not need thread sealant, and tape or paste on the stud thread can force the O-ring out of its groove. Over-tightening does not improve the seal and can stretch the thread or distort the port face. The stud end is torqued before welding and checked again only after the weld has cooled.
Installation Warnings
- ✔ Confirm the port is an ISO 6149-1 flat-face O-ring type before fitting this elbow.
- ✔ Fit a new O-ring of the tabulated size whenever the joint is broken.
- ✔ Hold the body steady and use a spanner on the S hex when breaking the joint.
- ✔ Shield the O-ring and stud end from weld heat, and weld only after the stud end is torqued.
- ❌ Never fit this elbow into a 24 degree cone port (DIN 2353 / ISO 8434-1), a 60 degree cone port, or a 74 degree cone / SAE J514 style port. The thread may start, but the seal geometry differs and the joint will not seal correctly.
- ❌ Never interchange this metric stud end with an inch O-ring stud end from the ISO 11926 family, even where thread diameters look close.
- ❌ Never use thread tape or sealant on the O-ring stud thread to stop a weep.
- ❌ Never weld with the O-ring fitted or with the stud end unsupported against heat distortion.
Applications and Industries
The 90 degree elbow metric male o-ring butt weld tube adapter 1EW9 appears wherever a machined port must turn a corner into a welded tube run.
- Cross-standard equipment integration. A block with ISO 6149-1 ports and a tube race built to DIN practice meet at a corner with no extra nipple and no second joint.
- Repair and replacement. Corrosion or stripped threads at a manifold corner are fixed by replacing the elbow rather than the block, with the cross reference service identifying the row from a sample.
- Power units and test rigs. Right-angle take-offs on valve blocks, accumulator brackets and test benches keep tube tight against the frame.
- Mobile and construction machinery. A welded elbow survives boom, outrigger and attachment vibration better than a stacked threaded joint, where a leak means downtime.
- Oil, gas, process and industrial plant. Stainless and plated options suit offshore, washdown and corrosive atmospheres with documentation for inspection regimes.
Tags: hydraulic adapter, metric O-ring stud end, ISO 6149 hydraulic fitting, butt weld tube elbow, 90 degree hydraulic elbow, weld-on hydraulic fitting, hydraulic manifold adapter, tube to port adapter.
OEM Customization and Quality Traceability
We manufacture matching hydraulic adapters and hose assemblies alongside our hose range, so specials are quoted engineering work rather than a favour. Laser marking of your part number, logo, date code and batch code is available on the body or the hex, and custom finishes, non-standard tube sizes, alternative O-ring elastomers and special body dimensions are quoted from your drawing or sample, normally within 24 hours.
Every batch is traceable from raw material to finished part. Batch records, dimensional results and material test reports are available with the goods, third-party inspection such as BV or SGS can be arranged, and finished assemblies are pressure tested with results recorded for the lot. Ordering the 90 degree elbow metric male o-ring butt weld tube adapter 1EW9 on a repeat schedule keeps one drawing, one O-ring size and one traceability record behind every corner of the circuit.
FAQ
Q: Is a metric male O-ring stud end the same as a DIN 2353 24 degree cone stud end? A: No. This stud end seals with an O-ring against a flat port face as defined by ISO 6149-2 in an ISO 6149-1 port, while a DIN 2353 / ISO 8434-1 24 degree cone stud seals on a cone machined inside the port. Thread sizes may look identical, but the sealing interface differs and the two must not be mixed.
Q: Can I use this elbow in a 74 degree cone port such as an SAE J514 style port? A: No. A 74 degree cone joint seals on a cone, not on a flat face with an O-ring, so a 1EW9 elbow will not seal there. Use a 74 degree cone adapter for that interface.
Q: What pressure can the 90 degree elbow metric male o-ring butt weld tube adapter 1EW9 take? A: The data sheet has no pressure column for this series, so the rating follows the port standard, the tube wall and the weld procedure selected, and the finished assembly is only as strong as its weakest member. Request a rating table for your combination and we will state the figure and the test method.
Q: What is the difference between the twelve rows? A: Only the thread size and the tube size. Each row pairs one metric stud thread with one tube outside diameter and lists the matching O-ring, L1, L2, D and S values.
Q: Why are two part numbers printed without the 9? A: The data sheet prints the two largest rows, 1EW-45-38 and 1EW-52-42, without the trailing 9 in the prefix. They belong to the same 90 degree weld-tube family and share its body and socket geometry.
Q: Which O-ring material should I order? A: NBR is standard for general mineral-oil hydraulic service across roughly -40 °C to +120 °C. Choose FKM for higher temperatures or chemically aggressive media, and tell us the fluid and temperature so the elastomer can be confirmed.
Q: Can you weld the tube on and ship a finished assembly? A: Yes. Tubing can be cut, welded and pressure tested to your drawing so the part arrives ready to install, which removes weld procedure work from your own shop.
Q: What is the smallest order and the lead time? A: Small quantities are accepted for samples and trials, standard rows are held for fast dispatch, and made-to-drawing specials are normally quoted within 24 hours with a lead time stated on the quotation.
Solicitar um orçamento
Send the port thread, the tube outside diameter, the tube wall and weld procedure, the material and surface treatment, and the quantity you need. To speed up a quotation on the 90 degree elbow metric male o-ring butt weld tube adapter 1EW9, add the drawing or a photograph of the port and the O-ring groove. We reply with part number, confirmed dimensions, price and lead time within 24 hours, and trial samples can be arranged at the same time.
Browse the full Hydraulic Adapters range for the complete family, or contact us to request a quote, mill test reports, and samples.


 English
 Spanish
 Portuguese
 French
 German