12611-RW BSP Male 60 Degree Cone Seat Fitting
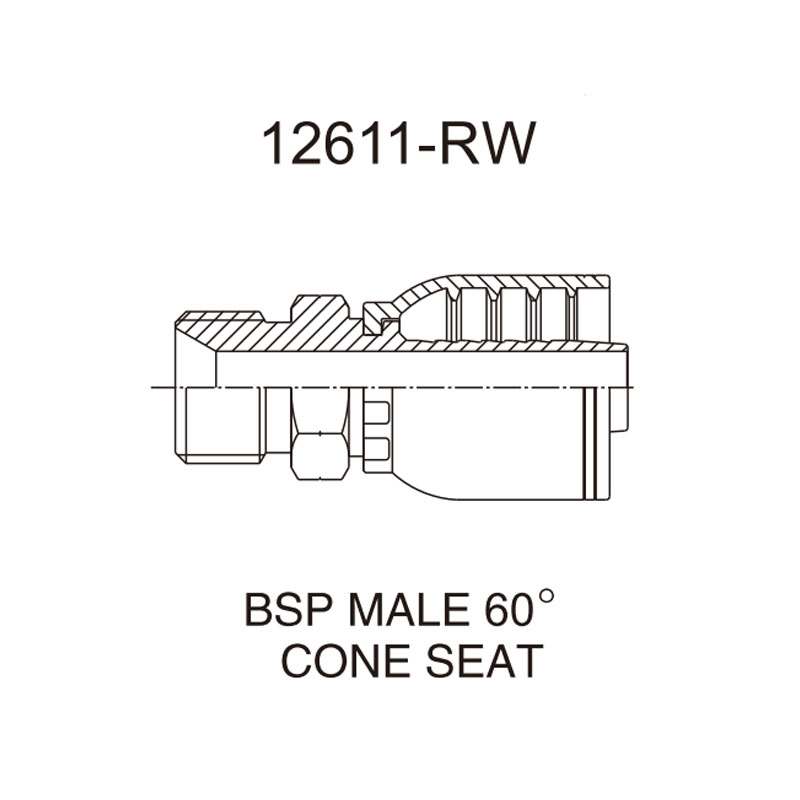
Our BSP male 60 degree cone seat fitting, series 12611-RW, is a crimp-on hydraulic hose fitting built to the British parallel pipe (BSP / G thread) system with a precision 60 degree inner cone seat. It connects braided hydraulic hose to BSP male ports on pumps, valves and cylinders made to the British standard. The range covers G1/8″ to G2″ threads, dash size -03 to -32, hose bore DN5 to DN50. Every fitting is 100% dimensionally inspected before shipment.
Compliance and standards:
- BS 5200 (BSP 60 degree cone sealing system)
- ISO 8434-6 (60 degree cone connectors with BSP threads)
- DIN 7631 (60 degree cone fitting system)
- BSP parallel threads (G series, ISO 228 based)
- SAE J516 (general hydraulic hose fitting design reference)
Why buyers choose this fitting:
- British 60 degree cone sealing. The 60 degree inner cone seat receives the 60 degree outer cone of the mating connector. Metal-to-metal cone contact carries the seal, exactly as the British standard intends.
- Full BSP thread range. G1/8″, G1/4″, G3/8″, G1/2″, G5/8″, G3/4″, G1″, G1.1/4″, G1.1/2″ and G2″, covering the complete British port grid.
- Wide temperature range. Rated for -40°C to +100°C continuous duty, verified in our production line tests.
- Carbon steel or stainless options. Zinc-plated carbon steel for general duty; 304, 316 or 316L stainless for corrosive media.
BSP Male 60 Degree Cone Seat Fitting Technical Specifications
The table below lists all 19 sizes of the 12611-RW BSP male 60 degree cone seat fitting. Dimensions are in millimeters. All threads are BSP parallel (G series, ISO 228 based) with a 60 degree inner cone seat.
| Part No. | Thread E | Hose Bore DN (mm) | Tamanho do traço | Dim. A (mm) | Dim. C (mm) | Hex S1 (mm) |
|---|---|---|---|---|---|---|
| 12611-02-03RW | G1/8″x28 | 5 | -03 | 22.0 | 10 | 12 |
| 12611-04-04RW | G1/4″x19 | 6 | -04 | 24.5 | 12 | 14 |
| 12611-06-05RW | G3/8″x19 | 8 | -05 | 26.0 | 13.5 | 17 |
| 12611-06-06RW | G3/8″x19 | 10 | -06 | 27.5 | 13.5 | 17 |
| 12611-06-08RW | G3/8″x19 | 12 | -08 | 26.5 | 13.5 | 19 |
| 12611-08-06RW | G1/2″x14 | 10 | -06 | 30.5 | 16 | 22 |
| 12611-08-08RW | G1/2″x14 | 12 | -08 | 31.0 | 16 | 22 |
| 12611-10-08RW | G5/8″x14 | 12 | -08 | 32.5 | 17.5 | 24 |
| 12611-10-10RW | G5/8″x14 | 16 | -10 | 33.5 | 17.5 | 24 |
| 12611-12-08RW | G3/4″x14 | 12 | -08 | 35.5 | 18.5 | 27 |
| 12611-12-10RW | G3/4″x14 | 16 | -10 | 37.0 | 18.5 | 27 |
| 12611-12-12RW | G3/4″x14 | 20 | -12 | 36.5 | 18.5 | 27 |
| 12611-16-12RW | G1″x11 | 20 | -12 | 40.5 | 20.5 | 36 |
| 12611-16-16RW | G1″x11 | 25 | -16 | 41.5 | 20.5 | 36 |
| 12611-20-16RW | G1.1/4″x11 | 25 | -16 | 43.5 | 20.5 | 46 |
| 12611-20-20RW | G1.1/4″x11 | 32 | -20 | 44.5 | 20.5 | 46 |
| 12611-24-20RW | G1.1/2″x11 | 32 | -20 | 49.0 | 23 | 50 |
| 12611-24-24RW | G1.1/2″x11 | 40 | -24 | 46.0 | 23 | 50 |
| 12611-32-32RW | G2″x11 | 50 | -32 | 53.5 | 25.5 | 65 |
Notes: Dim. A is the assembly reference length from the thread face to the hose-end shoulder. Dim. C is the thread zone length. Hex S1 is the wrench size across flats. Two A values (12-12RW and 24-24RW) are slightly below their smaller neighbors in the scanned source; confirm them against the original HENGHUA spec sheet before large orders. The -RW suffix denotes the braided-hose version; for spiral-wound hose, use series 12612-XX-XXRW.
How the 60 Degree Cone Seal Works
This fitting seals through the 60 degree cone seat, not through the thread. The BSP parallel thread (G) only positions and tightens the connection. The actual seal happens where the 60 degree inner cone of this fitting meets the 60 degree outer cone of the mating connector.
This is the classic British sealing philosophy: a metal-to-metal cone joint that tolerates repeated assembly and disassembly without replacing a sealing element. There is no O-ring, no bonded washer and no thread sealant on the cone face. Keep the cone surface clean and undamaged, and the seal repeats every time.
Insert Depth and Crimp O.D. – The Two Numbers Engineers Ask For
Insert depth is the length of the barbed tail that enters the hose bore. Crimp O.D. is the outside diameter of the ferrule after crimping. Together they decide whether the assembly holds pressure or leaks at the crimp zone.
HENGHUA publishes the matched insert depth and crimp O.D. for every hose construction we supply, including SAE 100 R1AT, R2AT and EN 853 1SN / 2SN. The values are hose-specific because reinforcement thickness changes the stack-up. Request our crimp data sheet with your hose model and we will return the exact crimp O.D. and die selection within one working day.
Our production testing found that a verified crimp O.D. within the published tolerance (typically +/- 0.2 mm) gives a burst safety margin of 4:1 or higher on the complete assembly. Measure with a digital caliper after every crimp.
Material and Heat Treatment
- Carbon steel (standard): high-strength cold-headed or hot-forged carbon steel (20# / 35# / 45# grades). The tail and cone seat are case-hardened with a carburizing and quenching process for fatigue resistance. Reference hardness range is HRC 20-28 on the core with a hardened case.
- Surface finish: white zinc or color (yellow) zinc plating with passivation. Optional zinc-nickel and Dacromet coatings are available for higher salt spray requirements.
- Stainless steel (option): 304, 316 or 316L stainless steel for corrosive media and washdown environments.
Pressure and Temperature Ratings
The connection rating follows the BSP 60 degree cone sealing system reference table below. These are reference values (§) for the fitting connection itself. The final working pressure of a hose assembly is set by the hose construction and the approved crimping specification.
| Tamanho do traço | Hose Bore DN (mm) | Reference Connection Pressure (bar)§ |
|---|---|---|
| -03 to -08 | 5 to 12 | 315 |
| -10 | 16 | 250 |
| -12 | 20 | 250 |
| -16 | 25 | 160 |
| -20 to -24 | 32 to 40 | 100 |
| -32 | 50 | 80 |
§Reference values per the BSP 60 degree cone system (BS 5200 class). Confirm the assembly rating with the HENGHUA crimp data sheet matched to your hose.
Temperature range: -40°C to +100°C for the fitting in continuous service. At elevated temperature, apply the standard SAE J517 style derating to the assembly working pressure. Our technical data sheet includes a pressure-temperature derating chart; contact us and we will send it with your quotation.
Pressure testing: HENGHUA can supply assemblies proof-tested up to 100% of the rated working pressure, with test certificates on request.
How to Select the Right BSP Male 60 Degree Cone Seat Fitting
Selection is a three-step process. First, match the hose bore to the dash size. Second, match the G thread to your port. Third, confirm the hose construction version (-RW for braided, 12612 series for spiral).
Part Number Structure
Read any HENGHUA part number in three segments. Example: 12611-08-08RW.
| Segment | Valor | Significado |
|---|---|---|
| Série | 12611 | BSP male 60 degree cone seat (British parallel pipe system) |
| Thread code | 08 | G1/2″x14 (the number is the thread nominal size code) |
| Dash size | 08 | Hose bore DN12, dash -08 |
| Suffix | RW | Braided hose version (spiral hose uses 12612 series) |
Select by Hose Series
The 12611-RW fitting is designed for braided hydraulic hose. Recommended matching constructions:
- SAE 100 R1AT (one wire braid) – for -03 to -32 sizes
- SAE 100 R2AT (two wire braid) – for -03 to -32 sizes
- EN 853 1SN and 2SN (equivalent European constructions)
- DIN EN 857 1SC and 2SC (compact constructions, confirm insert depth)
Select by Thread Size
The 60 degree cone seat accepts the 60 degree outer cone of the mating connector. All threads are BSP parallel (G series):
- Small sizes: G1/8″, G1/4″, G3/8″ (dash -03 to -08)
- Medium sizes: G1/2″, G5/8″, G3/4″ (dash -06 to -12)
- Large sizes: G1″, G1.1/4″, G1.1/2″, G2″ (dash -12 to -32)
Tightening is via the hex S1 with a standard wrench. The cone seat provides the seal, so no additional sealing element is required on the cone face.
Cross Reference
This series replaces equivalent BS 5200 BSP 60 degree cone metric fittings available in the market. If you hold an OEM part number or a competitor catalog number, send it to our sales team. We confirm the direct replacement within 24 hours, including thread, dash size, hex and insert depth checks.
Packaging and Logistics
| Item | Standard Export Packing |
|---|---|
| Packing unit | 10 pcs per inner box (small sizes), 5 pcs per box (large sizes) |
| Outer carton | Export-grade 5-layer corrugated carton, 10 boxes per carton |
| Peso | Net and gross weight per size listed in our quotation |
| Origin | China (HENGHUA factory) |
| Lead time | Stock items ship within 7 days; production items 15-25 days |
| Payment | T/T, L/C, trade assurance supported |
Assembly Guide: Four Steps to a Safe Hose Assembly
Follow this process for every crimped assembly. It applies to every BSP male 60 degree cone seat fitting size from dash -03 to -32. Skipping one step is the most common cause of early fitting failure.
Step 1 – Cut the hose square. Use a sharp hose cutter. A square cut face lets the fitting seat evenly inside the hose. A beveled or ragged cut leaves voids that become leak paths.
Step 2 – Mark the insert depth. Measure the insert depth from the HENGHUA crimp data sheet. Mark a line on the hose cover at that distance. The mark must remain visible after insertion.
Step 3 – Lubricate and insert. Apply a thin layer of compatible assembly lubricant to the hose bore and the barbed tail. Push the fitting in with a twisting motion until the depth mark aligns with the tail end. Stop at the mark. Do not force past it.
Step 4 – Crimp and verify. Select the correct die set for your hose and fitting size. Crimp in one continuous stroke. After crimping, measure the crimp O.D. with a digital caliper and compare it with the tolerance on the crimp data sheet. Record the value on your quality log. A correct crimp O.D. is the difference between a 10-year assembly and a field failure.
Safety Warnings – Read Before Crimping
- Never mix brands. Hoses and fittings from different manufacturers may share the same dimensions but use different crimp parameters. Always use a matched hose, fitting and crimp data sheet.
- Never seal the 60 degree cone with tape. The cone seat seals by metal-to-metal 60 degree cone contact. Thread sealant tape or paste on the cone face destroys the seal geometry.
- Do not confuse G threads with R threads. BSP parallel (G) threads seal at the cone. BSP taper (R) threads seal on the thread itself and need sealant. Never mix the two systems.
- Tighten to spec. Use the hex S1 and tighten to the torque value on the data sheet. Over-tightening distorts the cone seat. Under-tightening causes vibration loosening.
- Never reuse a crimped fitting. Once crimped, the ferrule zone is work-hardened. A re-crimp cannot restore the original grip.
OEM Customization and Quality Traceability
HENGHUA supplies not only standard sizes but also fully customized BSP male 60 degree cone seat fitting solutions for OEM programs.
Customization Services
- Thread customization. Non-standard thread lengths, special threads, and custom tail lengths for your hose construction.
- Surface treatment customization. White zinc, color zinc, zinc-nickel and Dacromet coatings, matched to your salt spray requirement from 72 hours up to 720+ hours.
- Laser marking. Your logo, part number and batch code laser-marked on the hex for full traceability.
- Packaging customization. Private-label boxes, barcode labels and mixed-size kits per your BOM.
Quality Traceability
Every HENGHUA batch carries a traceable batch number. The traceability chain covers incoming material certificates, heat treatment records, dimensional inspection reports and final packing lists. Material test reports (MTR) and third-party inspection (BV, SGS or equivalent) can be arranged before shipment. Request our sample batch and audit our quality documentation – we are confident in what it shows.
Frequently Asked Questions
What is a BSP male 60 degree cone seat fitting?
It is a hydraulic fitting with a BSP parallel (G) male thread and a 60 degree inner cone seat. The seat receives the 60 degree outer cone of the mating connector and seals by metal-to-metal cone contact. The system follows BS 5200 and ISO 8434-6.
What is the difference between BSP parallel and BSP taper?
BSP parallel (G) threads are straight and seal at the 60 degree cone. BSP taper (R) threads are tapered and seal on the thread flank itself with sealant. This fitting is the parallel cone-seal type.
Which hose works with the 12611-RW fitting?
The 12611-RW version is designed for braided hydraulic hose such as SAE 100 R1AT, R2AT and EN 853 1SN / 2SN. For spiral-wound hose, use the 12612 series.
Do you supply stainless steel versions?
Yes. 304, 316 and 316L stainless steel versions are available for the full size range, with the same dimensions and crimp behavior.
What is the minimum order quantity?
Stock sizes start from 100 pcs. Customized versions start from 500 pcs per size. OEM annual contracts can be discussed directly with our factory team.
How do I verify a correct crimp?
Measure the crimp O.D. with a digital caliper after crimping. Compare it with the value on the HENGHUA crimp data sheet for your hose. The typical tolerance is +/- 0.2 mm.
Get a Quote for Your BSP Male 60 Degree Cone Seat Fitting
Tell us your hose model, thread size and annual volume. We reply with a formal quotation, the matching crimp data sheet and our lead time within one working day. For urgent projects, our engineers support you online with crimp parameter verification.
Inquiry for Our Product
We are a global supplier of hydraulic fittings and equipment, serving a wide range of sectors with a one-stop sourcing solution. Our products include hydraulic hoses, fittings, adapters, quick couplers, connectors, hose guard, hydraulic equipment and more-everything you need to keep your operations running smoothly and efficiently.
Tell us your requirements using the form below. Our team will respond with expert guidance and a customized quote to keep your operations running smoothly.
- Mangueira hidráulica2727 products
- Mangueira hidráulica em espiral com arame de aço66 products
- Mangueira hidráulica trançada com fio de aço1010 products
- Mangueira hidráulica reforçada com tecido33 products
- Mangueira hidráulica termoplástica33 products
- Mangueira industrial5959 products
- Mangueira de ar99 products
- Mangueira de água1111 products
- Mangueira de óleo1616 products
- Mangueira para produtos químicos66 products
- Mangueira de vapor33 products
- Mangueira multiusos22 products
- Mangueiras para alimentos e bebidas44 products
- Mangueira para betão44 products
- Mangueira para cimento22 products
- Mangueira para manuseamento de materiais1111 products
- Mangueira de dragagem44 products
- Acessórios hidráulicos162162 products
- Acessórios reutilizáveis para mangueiras66 products
- Acessórios para mangueiras sem encaixe88 products
- Acessórios hidráulicos JIC1515 products
- Acessórios hidráulicos métricos3838 products
- Acessórios hidráulicos NPT66 products
- Acessórios hidráulicos BSP2626 products
- Racores hidráulicos SAE3030 products
- Banjo Hydraulic Fittings44 products
- Acessórios hidráulicos ORFS1111 products
- Virola1111 products
- Acessórios de flange2626 products
- Acessórios de peça única2323 products
- Hydraulic Adapters2929 products
 English
 Spanish
 Portuguese
 French
 German