A hose inspection program for chemical transfer is a documented cycle of scheduled visual examination, tagging, and a 1.5 × MAWP (maximum allowable working pressure) static pressure test that proves each assembly is fit for its next transfer.
This page sets out what a hose inspection program must prove, how often it should run, what an inspector looks at, how tagging and records work, and which KPIs a reliability team reports. It stays on chemical service, where compatibility, permeation, and static charge decide whether a hose is still fit. Numbers appear only where a published rule or a named standard supports them.
All pressure figures are working-pressure ratings at 23 °C ambient, and citations refer to the current text of the cited section rather than to a paragraph number. About 13 min read.
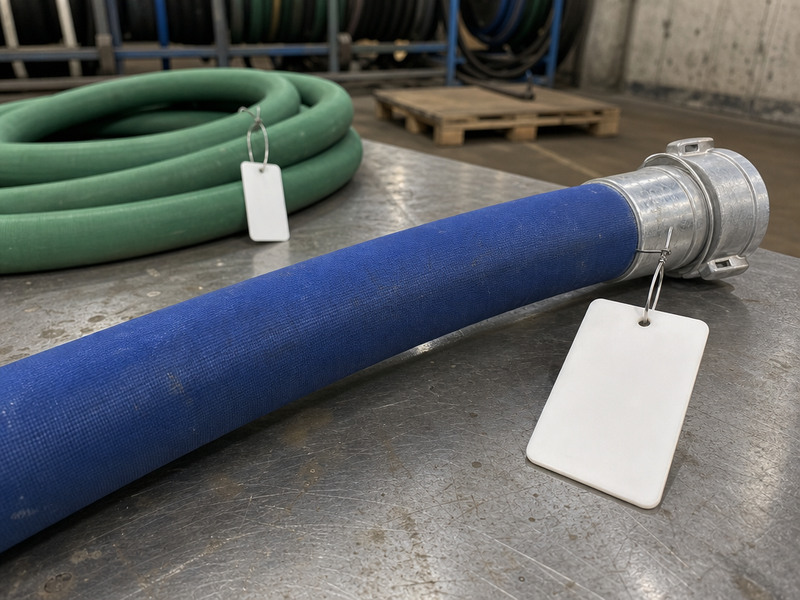
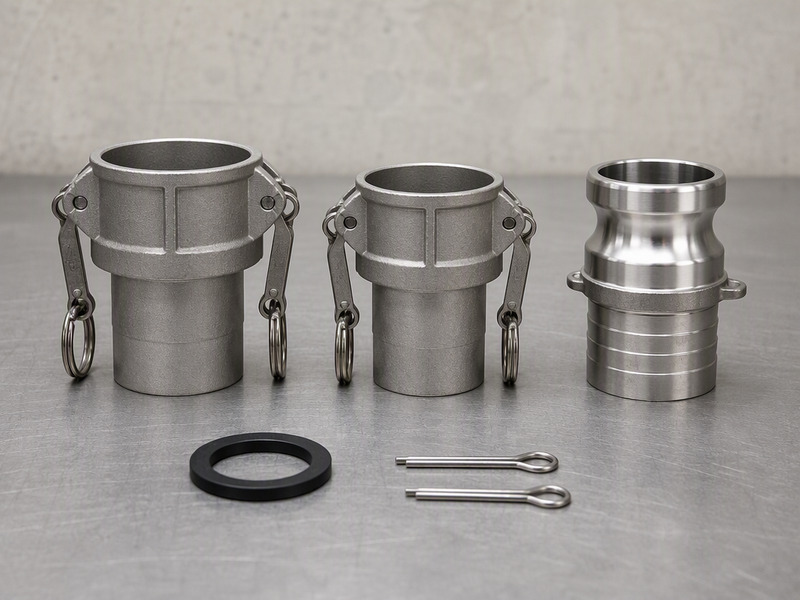
Figure 1. A hose inspection program begins at the bench, where clean, tagged chemical hose assemblies are staged before examination and test.
What Must a Hose Inspection Program Prove on Chemical Service?
A chemical hose rarely fails the way a general industrial hose does. The tube can soften, swell, or harden, the medium can permeate the wall and reach the cover, and static charge can build in a non-conductive assembly. The program exists to find those conditions before a transfer starts, not after product is on the ground.
The program must prove four things for each assembly. It must show that the construction still suits the medium, concentration, and temperature it will carry. It must show that the assembly is mechanically intact at both ends and along the bore. It must show that the assembly holds pressure without distortion. It must also show that the item can be identified, traced, and proven to be inside its test interval.
General condition checks are already covered in depth for hydraulic service, so this page does not restate that list. Where a program needs a general defect reference, start from the hydraulic hose inspection checklist and then add the chemical-specific points given below.
Construction is the first control, because the tube compound sets the chemical envelope. Rubber (EPDM and other compounds), UHMWPE, PTFE-lined, and thermoplastic composite builds each tolerate a different range of media, and the chemical hose collection lists the standard builds and their working pressures.
Two standards define the type designations used for chemical hose. EN 12115:2021 covers rubber and thermoplastics hoses and hose assemblies for liquid or gaseous chemicals, with Type D and Type SD assemblies, metal fittings, and four electrical grades. It allows a service range of -20 °C to +65 °C and working pressure up to 10 bar. EN 13765 covers thermoplastic multi-layer composite hoses in five types, with bores from 25 mm to 250 mm, working pressures from 4 bar to 14 bar, and working temperatures from -30 °C to +160 °C.
Neither standard replaces the manufacturer’s own compatibility data. Chemical resistance has to be checked against the specific medium, concentration, and temperature in the line, not against a family name. The program’s first inspection question is therefore whether this hose is still rated for what it will carry.
How Often Should a Hose Inspection Program Run?
Frequency is where many programs are weakest, because a single interval is applied to every hose. A hose bolted to a fixed transfer line, a hose coiled between jobs, and a hose carrying an aggressive medium do not share one safe calendar. The program should define at least two layers: a quick check before each transfer, and a documented inspection on a written interval.
Where a facility or a vessel transfers oil or hazardous material in bulk, the U.S. Coast Guard rules set a floor. Under 33 CFR 156.170 the pressure test is required annually for facilities and annually for vessels. The same section also allows a test not less than 30 days before the first transfer conducted more than one year after the last test. A site rule may be stricter than that floor, and where it applies it meets that floor at minimum.
The table below separates the routine check from the formal test, because the two produce different records and different owners.
Table 1. Layer, interval, and record for a chemical-service inspection program.
| Activity | Interval | Record produced |
|---|---|---|
| Pre-transfer visual check | Before every transfer, by the operator | Entry in the transfer or shift log |
| Documented visual inspection | Written interval set by the operator’s own risk assessment | Signed inspection sheet against the assembly code |
| Static pressure test | At least annually for facility and vessel transfers | Hose test certificate |
| Re-test after an abnormal event | After over-pressure, surge, impact, or a medium change | Incident-linked certificate and note |
| End-connection examination | With every documented inspection | Fitting and gasket condition line |
A written interval should also react to events rather than only to the calendar. An over-pressure, a surge, a dropped assembly, or a hose that has carried a new medium since its last test all justify an early re-test. Record that decision on the same sheet as the routine inspection, so the reason stays visible to the next inspector.
The Chemical Hose Inspection Checklist: What an Inspector Looks For
The chemical hose inspection checklist below follows the defect list that 33 CFR 156.170 applies to a nonmetallic transfer hose. It is written so that an inspector can mark each line pass or fail without having to interpret the wording.
- Cover and outer layer: look for unrepaired loose covers, kinks, bulges, and soft spots.
- Reinforcement and bore: look for gouges, cuts, or slashes that penetrate the first layer of reinforcement.
- External surface: check for deterioration such as cracking, blistering, and chemical staining.
- Internal condition: where both ends are open and the bore is visible, check for internal deterioration.
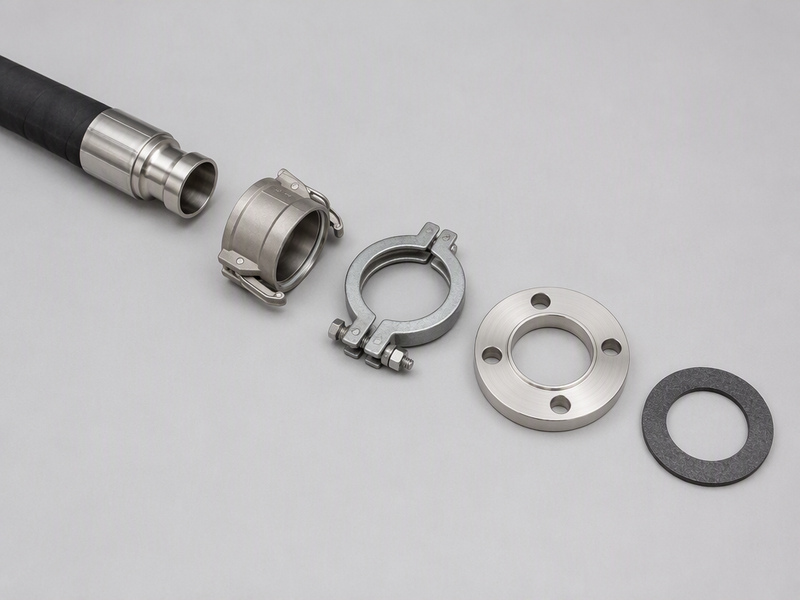
- End connections: inspect threads, flange faces, gaskets, camlock arms and pins, and the crimp or sleeve.
- Marking: confirm that the identification code and the MAWP remain legible.
- Compatibility: confirm the assembly still matches the manufacturer’s chemical resistance chart for the specific medium, concentration, and temperature.
Two further points matter on chemical service. First, the entire external surface must be accessible during the inspection and the test, so guards, covers, and insulation that hide the hose should be moved rather than worked around. Second, the checklist should confirm that any conductive or antistatic property the medium requires is still present, because that property is a construction feature that must be present as built.
In our own inspection reviews, the conductive or antistatic check is the line most often signed without a measurement. A visual pass cannot confirm it, so the sheet should carry a measured result there.
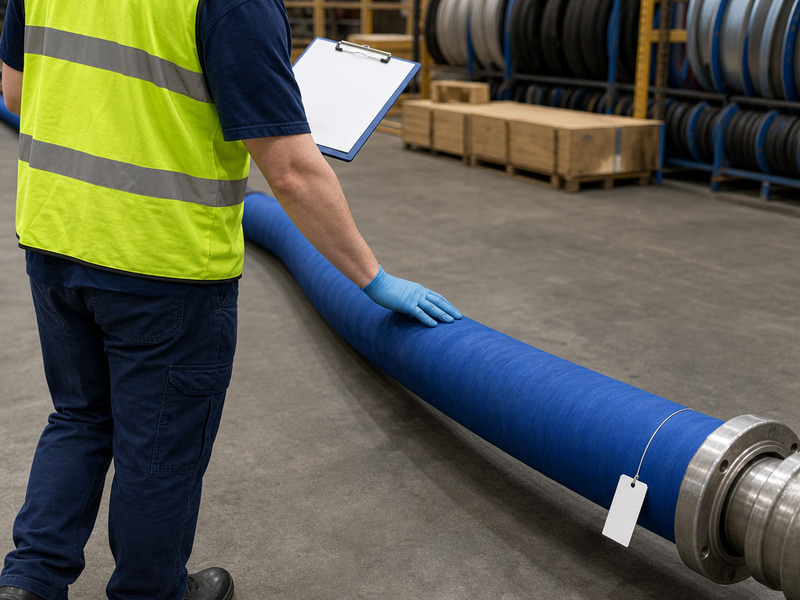
Figure 2. A hose inspection checklist is worked along the full length of the assembly, and every mark is recorded against the identification code on the tag.
Table 2. Defect, likely meaning, and the basis an inspector can cite.
| Finding | What it usually indicates | Basis |
|---|---|---|
| Loose cover, kink, bulge, or soft spot | A defect that could let product escape through the hose material | 33 CFR 156.170 |
| Gouge, cut, or slash into the first reinforcement layer | Reduced pressure-carrying capacity | 33 CFR 156.170 |
| External, or visible internal, deterioration | Ageing or chemical attack of the compound | 33 CFR 156.170 |
| Swollen or softened tube | Chemical incompatibility with the medium | Manufacturer’s chemical resistance chart |
| Cracked or lifted cover at the fitting | Stress at the end attachment or a permeation path | Assembly inspection record |
What Do Visual Hose Inspection Procedures Cover?
Run hose inspection procedures in a fixed order, so that no step is skipped when the transfer window is short:
- Isolate and depressurize the assembly, then drain it and, where the medium requires it, clean it before handling.
- Move the assembly to a level, well-lit area and remove covers so that the whole external surface can be seen.
- Check identification: confirm that the tag and the current MAWP match the assembly record.
- Walk the external surface end to end and mark every defect on the sheet as it is found.
- Open both ends and view the bore where the geometry allows it.
- Examine both end connections, including gaskets, threads, flange faces, and camlock hardware.
- Sign, date, and file the sheet, and change the tag status if the assembly is not returned to service.
Two people should sign any defect decision that removes an assembly from service. One inspector can miss a short run of damage on a long hose, and a second pair of eyes is cheap compared with an unplanned release. Keep the earlier sheets for the same identification code, so that a repeat finding shows up as a trend rather than as a surprise.
Hose Inspection Tags, Records, and Assembly Marking
Hose inspection tags are the field interface between a physical hose and its paperwork. A tag that travels with the assembly can show the identification code, the MAWP, the date of the last test, the next due date, and a status of in service, quarantined, due, or out of service. A missing or illegible tag is itself a program finding, because an untagged hose cannot be proved to be inside its interval.
The marking rules that apply to the service set what has to appear on the hose. Under 33 CFR 154.500 a hose must be marked with the product name, or with “OIL SERVICE”, or with “HAZMAT SERVICE—SEE LIST” plus a symbol keyed to a list in the operations manual. The same rule calls for the MAWP, the date of manufacture, and the date of the latest test. The last two may sit in the facility’s hose records instead, provided the hose is marked so that it can be identified.
One restriction catches people out. Burst pressure and test pressure must not be marked on the hose itself, even though both are held in the test record. That keeps a design figure out of the field, where a partial reading could invite a decision the inspection program should be making.
Table 3. Where each marking item may live under 33 CFR 154.500.
| 項目 | On the hose | In the facility hose records |
|---|---|---|
| Product, “OIL SERVICE”, or “HAZMAT SERVICE—SEE LIST” with keyed symbol | Required for the applicable service | Not a substitute |
| MAWP | Required | Supports the hose marking |
| Date of manufacture | Permitted | Permitted, if the hose is marked to identify it |
| Date of the latest test | Permitted | Permitted, if the hose is marked to identify it |
| Burst pressure and test pressure | Must not be marked | Held in the test record only |
The Hose Pressure Test: Static Proof at 1.5 × MAWP
The hose pressure test is the proof step of the program. Under 33 CFR 156.170, a nonmetallic transfer hose must not burst, bulge, leak, or abnormally distort under static liquid pressure of at least 1.5 × MAWP. Loading arms and transfer piping, including metallic hose, must not leak under at least 1.5 × MAWP. The test fluid must be a liquid compatible with the hose tube, as recommended by the manufacturer.
Scope of this test. The 1.5 × MAWP proof applies to nonmetallic transfer hose and to loading arms and transfer piping in the same service. An assembly in another service follows the rule for that service.
A test at 1.5 × MAWP is a proof test, not a burst test, and it does not replace the design margin built into the assembly. It confirms that the hose in front of you, as it stands today, holds the required multiple of its working pressure without changing shape. In our factory hydrostatic test, every assembly is pressurized to its rated working pressure before shipment, and the field test extends that same logic to the assembly in its working condition.
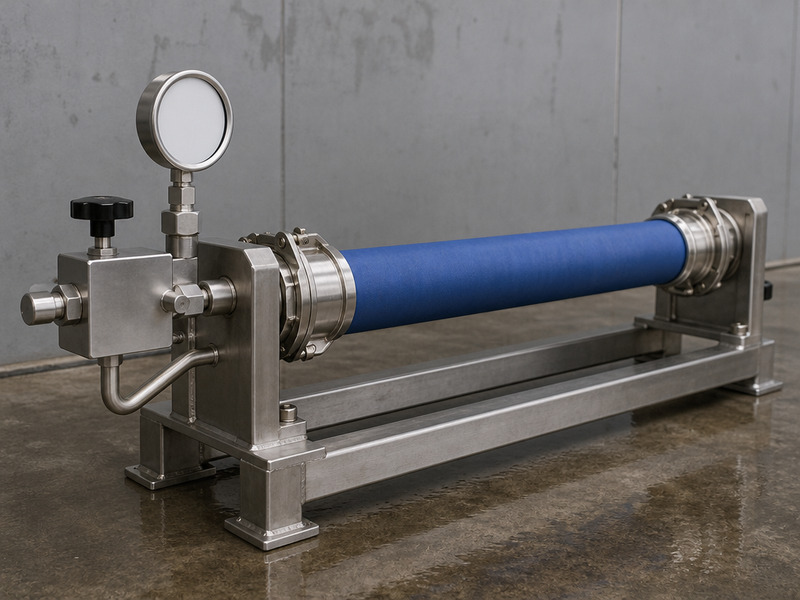
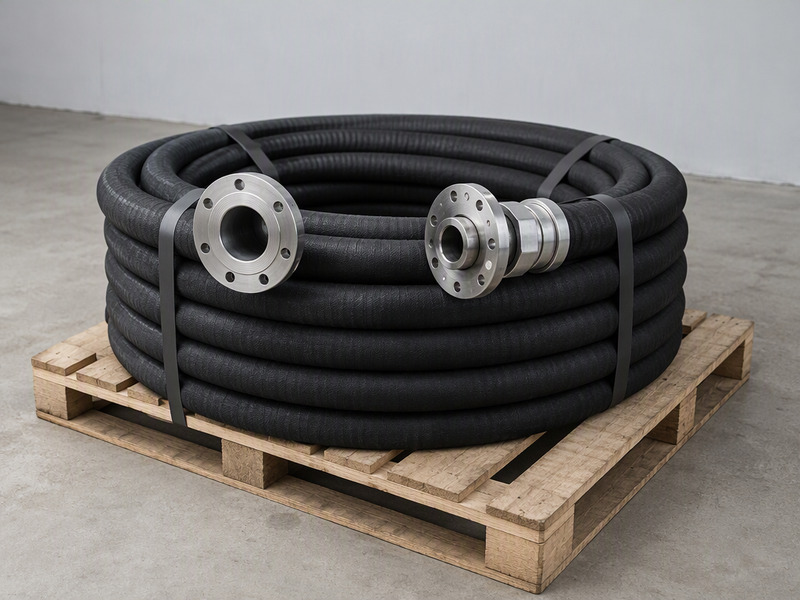
Figure 3. On the pressure test bench the assembly is held at 1.5 × MAWP while both end connections and the full cover are watched for leaks or swelling.
Prepare the test so that it proves something. The entire external surface must be accessible while pressure is held, so any cover that could hide a leak path comes off first. Hold the pressure long enough to watch the full length, both end connections, and every fitting, and watch for swelling as well as for drips.
Table 4. Test parameters for the static proof test of a chemical transfer hose.
| パラメータ | Requirement | Source |
|---|---|---|
| Test pressure | At least 1.5 × MAWP, as static liquid pressure | 33 CFR 156.170 |
| Acceptance | No burst, bulge, leak, or abnormal distortion | 33 CFR 156.170 |
| Loading arms and transfer piping | No leak at the same 1.5 × MAWP | 33 CFR 156.170 |
| Test fluid | A liquid compatible with the hose tube, as the manufacturer recommends | 33 CFR 156.170 |
| Accessibility | Entire external surface accessible during the test | 33 CFR 156.170 |
| Frequency | Annually for facilities and for vessels | 33 CFR 156.170 |
For the wider picture of how hydrostatic and impulse testing fit a standard series, including GB/T, ISO, and SAE practice, the guide to hydraulic hose testing and standards is a useful companion. Working pressure and burst pressure are different quantities, and the working pressure versus burst pressure comparison explains that relationship before a test pressure is set. End-connection hardware that the test exercises is covered in the guide to hose couplings and selection criteria.
What a Hose Test Certificate Must Record
A hose test certificate is the durable evidence that the test happened. It should identify the assembly, the pressure applied, the fluid used, the result, the date, and the person or station that ran it. Without those fields a certificate is only a form.
Run the certificate against a fixed field list:
- Assembly identification code, size, and MAWP.
- Test pressure applied, expressed as a multiple of MAWP.
- Test fluid and, where relevant, its temperature.
- Result: pass, or the defect that failed the assembly.
- Date of the test and the due date of the next test.
- Name or station of the person who ran the test.
- The inspection sheet that accompanied the test.
Keep the certificate with the assembly record, keyed by the identification code on the tag. When a customer or an auditor asks whether a specific hose was tested, the certificate should answer in one lookup. A certificate that cannot be matched to a physical hose by its code is a record-keeping defect in its own right.
Which KPIs Should a Hose Inspection Program Report?
A program that is not measured drifts. The indicators below tell a reliability team whether the program is working, without turning inspection into a numbers game. Report the trends, and treat an unexplained jump as a signal to look at the cause rather than at the target.
Table 5. Key performance indicators a chemical-service inspection program reports.
| Indicator | What it tells you | Reporting form |
|---|---|---|
| Inspection completion rate | Whether scheduled inspections actually happened | Share of due inspections closed |
| Test pass rate | Share of assemblies that pass the 1.5 × MAWP test first time | Percentage, by medium and by line |
| Findings by defect class | Which defect types are rising | Count per category per period |
| Overdue assemblies | Exposure from hoses held past their next due date | Count of tags past due |
| Repeat findings | Whether the same assembly keeps failing | Count per identification code |
| Certificate coverage | Whether every in-service hose has a current certificate | Percentage of in-service assemblies |
Round the set out with one friction measure and one coverage measure. A pass rate that falls while coverage stays high points to a medium or a supplier problem. Coverage that falls while the pass rate stays high usually points to record-keeping rather than to hoses, and that is a different fix.
From Inspection Finding to the Right Next Step
A finding has to become an action: re-test, repair, derate, or retire. The decision rule belongs with the people who hold the budget, so it is worth writing the thresholds into the program before the first failure rather than after it. Maintenance scheduling, storage, and the lifecycle cost model are covered in hose maintenance in chemical plants, and root-cause analysis of a failed assembly is a separate method with its own evidence trail.
Out-of-service boundary. Take the assembly out of service when the cover is worn through to the reinforcement. The same applies when the bore keeps a kink, bulge, or soft spot, when the tag code is no longer legible, or when it fails the 1.5 × MAWP test. Each of those is a positive stop condition, and the assembly returns to service only after it has passed a repeat test.
Table 6. Finding, disposition, and the tag and record that follow.
| Finding | Disposition | Tag and record |
|---|---|---|
| Cover mark, no reinforcement exposed | Return to service, note the location | In service; line on the sheet |
| Kink, bulge, or soft spot | Quarantine and re-test before transfer | Quarantined; re-test required |
| Cut into the first reinforcement layer | Remove from service | Out of service; retirement note |
| Failure of the 1.5 × MAWP test | Remove from service and record it | Out of service; linked certificate |
Chemical Transfer Hose Inspection Program FAQs
How often does a chemical hose need a pressure test?
Under 33 CFR 156.170, facilities and vessels must pressure-test transfer hoses annually, and a test is also required not less than 30 days before the first transfer conducted more than one year after the last one. A site may set a shorter interval. Between tests, keep a documented visual check in the program, because damage can occur between the annual dates.
Does a visual check replace the pressure test?
No. A visual inspection finds what can be seen, such as loose covers, kinks, bulges, or a cut through the reinforcement. A hose pressure test finds defects that appear only under load, such as a slow leak at a fitting or distortion as pressure rises. A program needs both, and each produces a different record.
What does the 1.5 × MAWP static test actually prove?
It proves that the assembly, in its current condition, holds at least one and a half times its maximum allowable working pressure without bursting, bulging, leaking, or abnormally distorting. The test uses a static liquid pressure and a fluid compatible with the hose tube, as recommended by the manufacturer. It is a proof test at the required multiple of MAWP, not a measure of burst strength.
What is the difference between a hose tag and a test certificate?
Hose inspection tags travel with the assembly and show the identification code, the MAWP, the test date, and the status at a glance. The hose test certificate is the signed record of the test itself, filed and matched to the tag by code. The tag is the field reference and the certificate is the durable evidence, so a complete program keeps both.
Which records does the program have to keep?
Keep the inspection sheet, the pressure test certificate, and the assembly record for each identification code. Under 33 CFR 154.500, the date of manufacture and the date of the latest test may be held in the facility’s hose records instead of on the hose, provided the hose is marked so that it can be identified. A record that cannot be matched to a physical hose by its code is a defect in the hose inspection program.
Can one hose inspection checklist cover every chemical hose?
Not entirely. The physical-condition lines can be shared, but the compatibility decision cannot. Each assembly has to be checked against the manufacturer’s chemical resistance chart for the specific medium, concentration, and temperature it will carry. A medium change, a concentration change, or a temperature change can invalidate an earlier decision, so the checklist should carry a line for that review.
How should findings be recorded so that they stay useful?
Record each finding against the assembly identification code, with the date, the defect class, and the action taken. Keep the earlier sheets for the same code so that a repeat finding shows up as a trend. A short coded defect list is better than free text, because it lets a reliability team count findings by category and see which medium or line is producing them.
Who can run the pressure test?
The rule sets the test conditions, not a job title. What matters is that the person can control the pressure accurately, hold it while the whole external surface is watched, recognize distortion as well as leakage, and sign the result. A distributor workshop and a site workshop both qualify when the equipment, the written procedure, and the record are controlled.
Do the procedures change for a new assembly?
The hose inspection procedures stay the same, but the baseline changes. For a new assembly, add the factory test record and set the first due date. Treat the shipment test as a starting point rather than as a permanent pass. From the first day in service the assembly needs a tag, an interval, and a certificate trail, so that later tests can be compared with a known baseline.
What happens to a chemical hose that fails its pressure test?
A failed chemical hose comes out of service and stays out until the fault is cleared and a repeat test is passed. The failure is recorded against the identification code, with the test pressure, the defect, and the disposition. The hose inspection program reports it as a finding class, so a run of failures on one medium becomes visible.
Closing: Running a Hose Inspection Program You Can Audit
A program earns its place when an auditor, a customer, or an incident investigator can follow it from the tag to the certificate. The floor is set by the rules above: a documented frequency, a real inspection, a legible tag, a matched certificate, and a 1.5 × MAWP test that the records support.
Before the next program review, confirm the essentials:
- A written interval exists for both the routine check and the static test.
- Every in-service assembly carries a legible tag with a current identification code.
- A certificate on file matches each tag to a test date.
- The 1.5 × MAWP test is run with an accessible surface and a compatible fluid.
- KPI trends are reported on a fixed cycle, not gathered only after a failure.
HENGHUA manufactures chemical hoses, chemical hose assemblies, industrial hoses, and hose fittings for distributors, EPC contractors, and OEM brands worldwide. Chemical hose construction covers rubber (EPDM and other compounds), UHMWPE, PTFE-lined, and thermoplastic composite builds.
Assemblies are terminated with crimped, swaged, or banded hose ends, flanged ends to ASME or EN patterns, and cam and groove (camlock) couplings, in carbon steel, 304/316 stainless steel, aluminum, brass, and PP/PVDF where the medium demands it. Every assembly is hydrostatically tested to its rated working pressure before shipment, and marked with its MAWP, size, and identification code. Commercial terms include factory-direct pricing, short lead times for bulk orders, private labeling, custom packaging, OEM/ODM branding, and warranty.
To build a program around a known assembly, or to compare factory test data before you buy, request a quote and samples from our engineering team.
About the author. The HENGHUA engineering and quality team designs and pressure-tests chemical hose assemblies for chemical, petrochemical, and marine transfer service. This page draws on our factory hydrostatic test practice and on assembly records from distributor inspection programs, and it follows the published U.S. Coast Guard transfer rules and the named hose standards. Questions about a specific medium, size, or end connection are answered by the same team that builds and tests the assemblies.
 English
 Spanish
 Portuguese
 French
 German
 Arabic
 Russian
 Indonesian
 Japanese
 Korean