
A steam hose inspection program turns hose care into a routine: every assembly is identified, inspected on a schedule, tagged, and retired on evidence. It finds damage while the line is cold and the area clear, not when a pinhole is already cutting steam across a walkway, and it converts the finding into a replacement booked inside a window.
This guide explains why planned inspection pays, how to set inspection intervals by duty, what a workable checklist contains, and how tagging and records feed maintenance planning. The scope is industrial hose in plants generally, with saturated steam as the driving case. Fire service hose and hydraulic circuits follow their own inspection rules. The daily habits performed at the workstation are a separate job, covered in task-level steam hose maintenance.
All pressures are gauge pressures; saturated-steam temperatures are the saturation temperature at that pressure. About 16 min read.

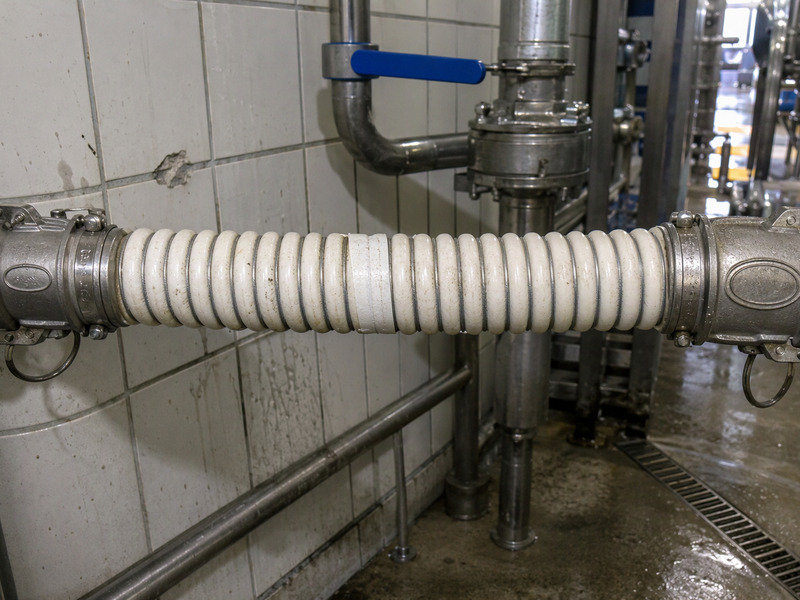
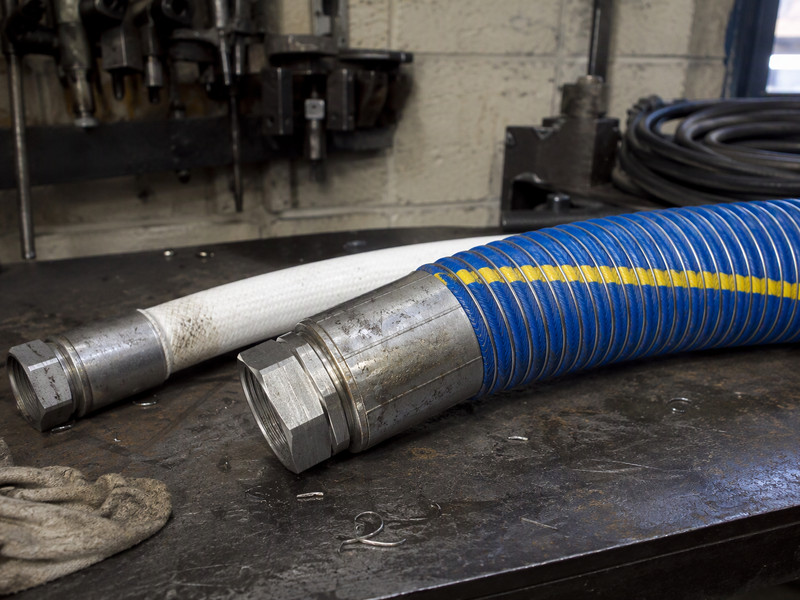
Figure 1. A steam hose inspection program identifies every assembly, inspects it on a schedule and records what the inspection found.
Why a Steam Hose Inspection Program Beats Reactive Repair
Reactive repair starts with a failure and ends with a story about a hose that “went suddenly.” Proactive inspection starts with a register and ends with a planned replacement inside a scheduled window. Only one of those two outcomes can be planned around.
The cost difference shows up mostly as availability. A hose that fails mid-shift stops the line, exposes anyone nearby to steam, and pulls the crew off planned work at the worst moment. A hose found at inspection is cold, isolated and already inside a maintenance window.

Figure 2. Planning board used to place hose replacement work into scheduled maintenance windows.
Table 1. Reactive repair compared with a planned steam hose inspection program
| Aspect | Reactive repair | Planned inspection |
|---|---|---|
| When damage is found | After the failure | At the inspection or the pre-shift check |
| Who finds it | Whoever is nearest | The person named in the plan |
| Line availability | Lost without notice | Replacement booked in a window |
| Safety exposure | Steam released near people | Damage found while the hose is cold |
| Spares | Emergency purchase | Correct assembly already in the store |
| Records | Memory and guesswork | Dated inspection and defect history |
| Effect on planning | An unplanned constraint | An input to the schedule |
The second column depends on one habit: writing down what you saw. An inspection that ends in a verbal report is a conversation, not a program. A dated sheet with a defect code is what turns a repair into a replacement forecast.
Cover damage and permeation behave the way they do because of the tube compound and the reinforcement build, so the site’s material guidance is the right companion to this page. For that background, see EPDM steam hose for saturated steam.
Setting Hose Inspection Frequency by Duty
Intervals should follow how hard a hose works, not how long it has sat in the store. Duty, pressure, temperature, movement and routing decide how quickly an assembly consumes its useful life. One annual date applied to a whole plant ignores all five; a tag date per assembly, adjusted by duty, is the version that survives a review.
Table 2. Hose inspection frequency by duty for steam and industrial hose
| Duty | Starting interval | Inspected by | Shorten the interval when |
|---|---|---|---|
| Saturated steam to 6 bar, fixed run | Weekly visual, quarterly full | Shift fitter | Any cover blister or weeping mark |
| Saturated steam to 18 bar, fixed run | Each shift visual, monthly full | Shift fitter and planner | Any coupling movement or restriction fault |
| Steam hose on moving equipment | Each shift visual | Operator | Any abrasion mark on the cover |
| Steam hose routed outdoors or near radiant heat | Weekly visual | Shift fitter | Cover hardening or sun exposure |
| Industrial hose carrying water, air or slurry | Weekly visual, quarterly full | Area technician | Kinking, crushing or wear at a support |
| Any hose after a hammer event or a repair | Before return to service | Named inspector | Treat every case as a special check |
That interval column is a starting position for the plan, not a standard. Three months of findings will tell you whether a line is over-inspected or under-inspected, and the register will show which answer is right.
Two extra rules tighten the loop. A hose that has been offline for more than a week is inspected before it returns to service. A hose that has been rerouted or re-terminated is inspected on the first shift after the change.
Where a line runs at 18 bar, the saturated-steam temperature is around 210 °C; at 6 bar the same duty sits near 165 °C. Pressure, not a separate temperature setting, sets what the hose sees. Which type envelope that pressure puts the assembly in is set out in the ISO 6134 type and class guide.
A Hose Inspection Checklist That Works on the Floor
A checklist earns its place only if a fitter can finish it between two jobs. Eight lines is workable; forty lines will be signed without being read. The point is to catch the findings that stop a hose.
The floor checklist used on steam duty covers these points, in this order:
- Identity: the tag is readable and matches the register entry.
- Cover: blisters, bulges, cuts, hardening or a flattened section.
- Perforations: the pin-pricked cover is open, not painted over or taped.
- Reinforcement: no textile or wire showing at bends, clamps or frame edges.
- Couplings and ferrules: no slippage, no rust weeping, no cracked swage.
- Restraint: cable or whip check fitted correctly and not chafing the cover.
- Routing: no kink, crush point, hot surface or sharp edge in contact.
- Leak evidence: stains, dried salts or a damp patch under the assembly.
A finding that points to a permeation path, exposed reinforcement or a moving coupling stops the hose; a mark that stops at the cover goes to the plan. That rule keeps the checklist from turning a small mark into an argument at the bench, and keeps the critical items visible on a short-handed shift.
The scope of the check is an assembly that is isolated, depressurized and at ambient temperature. A cover still hot to the touch is cooled first. Superheated steam and trace heating above the saturated-steam envelope need the supplier’s own limits.
A full eight-line check runs at the pace of access rather than the pace of the sheet. One hose behind a guard or under insulation takes longer to expose than to inspect, which is why the route is planned by area.
Write the finding beside the item rather than in a separate report. A sheet with a space for the defect code is faster to audit than a clean page with a separate narrative. Codes also make the monthly tally possible without reading every comment.
Table 3. Finding codes that keep floor notes short and auditable
| コード | Finding | Action | Record |
|---|---|---|---|
| A1 | Cover blister or bulge over a permeation path | Remove from service | Photograph and close the tag |
| A2 | Reinforcement exposed at a bend or a clamp | Remove from service | Photograph, note the contact point |
| A3 | Coupling slippage or rust weeping at the swage | Remove from service | Note the hours run and the duty |
| B1 | Surface cut or abrasion with no reinforcement damage | Monitor, reroute at the next window | Photograph and date it |
| B2 | Restraint chafing the cover | Refit the restraint | Note the fitting change |
| B3 | Dried salt or staining at a fitting | Re-torque or re-terminate | Note the action taken |
Replacement assemblies should come from the same steam hose collection so the pressure class, bore and end connection match the line. For the wider list of failure signs and the inspection procedure behind them, the existing hose inspection checklist for fifteen failure signs transfers to steam once the temperature and drainage rules are applied.
The Hose Tag System in Practice
A tag is the hinge between the hose on the rack and the record in the office. Without one, an inspection finding belongs to an anonymous length of rubber. With one, the same finding becomes history that somebody can act on.
Four items make a tag work at arm’s length: a unique number, the assembly specification, the date it entered service, and the date and result of the last inspection. The remaining fields live in the register and reach the tag through the number. Anything longer than four lines becomes unreadable after a month in a steam bay, and legibility matters more than detail.
Metal survives steam areas better than paper or adhesive. A stamped stainless plate wired to the ferrule stays readable for years, while a printed label lifts within weeks. If the tag cannot be read, the hose is effectively untagged.
The hose tag system should also record the inspector’s initials, because a name creates more care than a tick. A date beside the initials is enough to trace a decision later, and costs nothing on the floor. Initials also set the control on a removal: an A-code takes the hose out of service on the inspector’s signature, and the register keeper countersigns in the same shift, so an assembly cannot sit in the bay while its line stays connected.

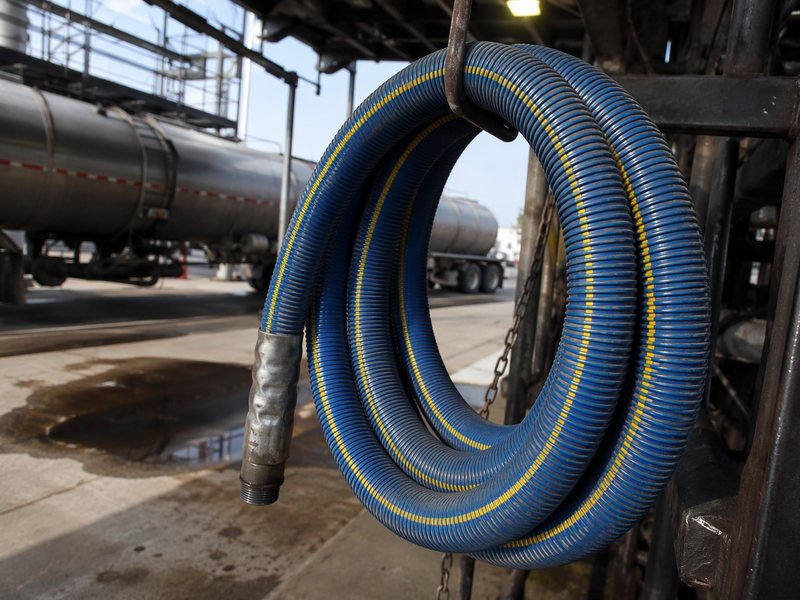
Figure 3. A stamped stainless tag on the ferrule carries the assembly number, the specification and the last inspection date.
Table 4. Data recorded against a hose tag and where each item is used
| Field | Typical format | Used for |
|---|---|---|
| Assembly number | Plant code plus serial | Finding the register entry |
| Bore and length | Millimeters and meters | Matching a replacement |
| Pressure class | Rated working pressure | Confirming the duty is legal and safe |
| Standard envelope | ISO 6134 Type 1 or Type 2 | Checking the assembly against the duty |
| Ends | Coupling type and material | Correct spares and tooling |
| Date in service | Month and year | Age at the review point |
| Last inspection | Date, initials and result | Frequency control and audit |
| Next due | Date or interval code | Building the weekly route |
Records and Hose Management: What to Keep
Hose management is a records discipline before it is a technical one. The technical findings are usually easy to see; keeping them retrievable years later is the difficult part. A register that cannot be searched is a stack of paper.
The assembly register, the inspection sheets, the defect photographs and the disposal notes sit in one place, keyed to the tag number. Every item has to be findable from the number on the hose. If the number is the only key, the filing rule is trivial.
The assembly register is also the basis for stock decisions. When a third of the fleet falls due in the same quarter, the buyer needs to see that coming months earlier. Records turn a surprise into a purchase plan.

Figure 4. Inspection sheets keyed to a tag number, filed with photographs and disposal notes.
The record set that supports the route is smaller than most teams expect:
- A register of assemblies with tag number and specification.
- Inspection sheets with date, inspector and defect code.
- Photographs of every A-code finding before removal.
- A replacement and disposal log with the reason.
- A note of restraint and fitting changes made on site.
- Evidence of the pressure check after any re-termination.
Two questions decide whether the filing survives a busy quarter. Who updates the register when a hose is swapped, and where the sheet goes at the end of the shift? Answer both in the written procedure, not in conversation.
In most registers we see, the finding with no record behind it is a hose swapped during a breakdown. The new assembly went in and the register kept the old number. Every later inspection then attaches to an assembly that is no longer on the line.
Industrial Hose Inspection: Widening the Program Beyond Steam
Industrial hose inspection uses the same loop as steam, but the failure modes change with the service. What changes is what you look for and how often you look. The register, tags and codes stay exactly as they are.
On steam, the drivers are temperature, condensate and permeation through the tube wall. On water and slurry duty, abrasion and support wear lead the list. On compressed air, kinking, fitting damage and impact damage dominate the findings.
Widening the route also widens the return, because one inspection walk can cover a whole plant instead of one steam bay. Start where the risk sits, then extend along the natural path of the shift. A wider route needs a decision on scope first, which is where types of industrial hoses and how to choose the right one helps frame the categories.
Table 5. What changes when industrial hose inspection covers other services
| Service | Main damage driver | Check that matters most | Extra caution |
|---|---|---|---|
| Saturated steam | Heat, condensate, permeation | Cover blisters and perforation condition | Isolate and cool before inspection |
| Hot condensate return | Cycling and water hammer | Restraint and coupling movement | Drain before opening |
| Compressed air | Kinking and impact | Cover cuts and fitting security | Store pressure after shutoff |
| Water and washdown | Abrasion and drag wear | Cover thinning at contact points | Slippery walkways |
| Slurry and material handling | Internal wear and crushing | Bore wear and kink marks | Weight and lifting aids |
| Chemical transfer | Permeation and swelling | Cover softening and odor | Refer to the compatibility data |
One caution applies across all six services. The inspection standard for a hot, moving or heavy hose is not the same as the standard for a light hose on a bench. Set the interval from the duty, not from the tag age, and review it when the duty changes.
Linking Inspection Findings to Maintenance Planning
Findings only pay when they change a plan. An inspection sheet that stays in a folder is a compliance artifact rather than management. The step that matters is the monthly reading of the codes.
Aggregate the defect codes once a month and look for repeats. A single kink is an accident; six kinks along the same line is a routing problem that a new hose will not solve. Repeat findings are where inspection turns into engineering.
Three numbers show whether the program holds: the share of due inspections closed on time, the count of repeat findings at one position, and how often the replacement is missing on its due date. Report them beside the monthly code tally, because an unmeasured program drifts. A fall in the first number is a scheduling problem before it is a discipline problem.
Two planning outputs matter most. The first is a replacement date on the maintenance calendar, so the work lands in a window instead of a breakdown. The second is the spares list that keeps the correct assemblies in the store.
Planned replacement also feeds inventory. Rationalizing assemblies into fewer sizes cuts holding cost and makes the register easier to keep current, as set out in reducing hose inventory costs through SKU rationalization.
Service life is consumed at a different rate on every line, so the hose maintenance and service life guide is more useful as a method than as a fixed interval. Use it to challenge the interval, not to replace the inspection.
Rolling Out a Steam Hose Inspection Program
A steam hose inspection program should start with one steam bay and one shift. The first version has to be deliberately small, because the plan that survives is the plan that was tested on the floor. Ambition added later is cheap; credibility lost early is not.
Expect the first pass to produce more findings than the plan can absorb. That is normal, and it is the argument for doing one area properly instead of every area badly. The register gains value from depth rather than breadth.
Eight steps are enough to stand the route up:
- List every hose in the area and apply a tag number.
- Write the checklist for steam duty and have it printed.
- Set the starting interval from the duty table.
- Name one inspector per shift and one keeper of the register.
- Run the first full inspection and record findings with photographs.
- Review the findings after thirty days and adjust the interval.
- Put the replacement dates onto the maintenance calendar.
- Extend the route to the next area once the first one holds.
Keep the first month blunt: inspect, record, fix the critical items, and leave the cosmetic list for the next window. The second month is where the interval becomes honest, because by then you have data instead of assumptions.
The first version also differs in three settings. A single-bay plant with no maintenance system runs the register on the tag and one sheet. A multi-line plant with a maintenance system keeps the interval on the asset record. A distributor keeping a register for customer sites needs one numbering rule that survives the trip between warehouse and plant.
Steam Hose Inspection Program FAQs
What changes when a plant stops only repairing failed hoses?
A failed hose stops being the trigger. Work moves to a date that maintenance controls, so the hose is replaced while the line is already down for another reason. Spares are ordered before the failure rather than after it. The practical gain is availability and a shorter list of surprises.
How often should steam hoses be inspected?
Start with the duty, not the calendar. A hose on continuous saturated steam at high pressure is checked each shift and fully inspected monthly; a light indoor run can start at weekly visual checks with a quarterly full inspection. There is no single correct hose inspection frequency, so set a starting interval and let three months of findings move it.
Can one checklist cover every hose in the plant?
It can, if the list stays short. A single hose inspection checklist with about eight floor lines works for steam and can be adapted for water, air or slurry by swapping two or three items. The structure stays the same: identity, cover, reinforcement, fittings, restraint, routing and leak evidence.
What information belongs on a hose tag?
Four items carry most of the value: a unique assembly number, the specification including bore, length and rated pressure, the date the hose entered service, and the last inspection date with its result. Inspector initials are a useful fifth. A hose tag system with those fields supports tracing, replacement matching and frequency control without becoming a data sheet.
Should inspection findings be photographed?
Photograph every finding that removes a hose from service, and anything you cannot describe in one line. A photograph settles arguments about cover blisters, coupling movement and contact damage long after the hose is gone. Date the file and link it to the tag number so it can be found in a later review.
Can the same route cover non-steam hose services?
Yes, and it usually should. The register, the tag and the defect codes work for every hose in the plant; only the check points and the interval change with the service. Adding air, water, slurry or chemical hoses to the same walk costs a little shift time and widens the value of the records.
Who should be accountable for the hose register?
A named person, not a department. One keeper should own the register, issue the tags, review the defect codes monthly and book replacements into the maintenance plan. Inspectors can be shift staff, but the keeper closes the loop. Hose management shared informally between two people usually stops being updated within a month.
What stops crews from following the checklist?
Usually three things: the sheet is too long, the findings lead nowhere, and nobody signs the register. Trim the list to the items that change a decision, act visibly on the first batch of findings, and put a name against the record. A crew that sees a kink fixed and a routing changed keeps filling in the sheet.
Does a scheduled inspection program remove the need for pre-shift checks?
No. The scheduled inspection is deeper but less frequent, while the pre-shift check is quick and sits with the operator who starts the line. The two catch different things. Inspection finds what time has done to the assembly; the pre-shift check finds what happened since the last shift, such as a kink, a moved restraint or a fresh damp patch.
What is the difference between an inspection program and a maintenance schedule?
A schedule lists when work happens. A program also decides what counts as a pass, who signs, what the record proves and when the hose leaves service. The schedule is the calendar layer. A plant can hold a clean schedule and still fail an audit, because a sheet shows dates but not decisions.
Can a steam hose be inspected while the line is still hot?
The check is run on an isolated, depressurized and cooled assembly, never on a live line. A hot cover hides the evidence the inspector is looking for, and a pressurized hose puts the inspector within reach of a release if a coupling moves. Book the check on the cold side of a shutdown.
How do inspection findings reduce downtime?
They move the repair into a window the plant already controls. A hose replaced during a planned stop costs the production time of that stop, not a full unplanned outage. Findings also expose repeats, such as six kinks on one line, which point to a routing fix rather than another hose. Both effects show up in unplanned downtime.
Final Verdict: Starting a Steam Hose Inspection Program
Start with one hose and one page. Tag it, inspect it on a set interval, write down what you found, and repair the critical finding before the next shift. That single loop contains everything the full route will later do at scale.
The first week is enough to prove the idea:
- Choose one bay and one steam line.
- Give every hose a number and a visible tag.
- Print one checklist and one defect code sheet.
- Name the inspector and the record keeper in writing.
- Book the first replacements into the next planned window.
A steam hose inspection program then grows by area rather than by ambition, and every area added makes the register more useful than the last. The aim is not a perfect document. It is a cold hose, found early, replaced on schedule, and never the reason a shift stops.
HENGHUA manufactures steam hoses, steam hose assemblies, industrial hoses and hose fittings for distributors, EPC contractors and OEM brands. The steam range uses an EPDM tube with textile or steel-wire reinforcement and a perforated, oil-resistant cover. Bore sizes and pressure classes cover the ISO 6134 Type 1 and Type 2 envelopes.
A high-temperature grade rated to 230 °C covers duties above the saturated-steam range. Assemblies are terminated with bolted safety clamps, crimped or swaged ferrules, flanged ends and cam and groove couplings. End materials include carbon steel, 304 or 316 stainless steel and brass.
Every assembly is hydrostatically tested to its rated working pressure before shipment. Each hose is marked with its size, working pressure and identification code. Factory-direct pricing, short lead times for bulk orders, private labeling, custom packaging and OEM branding are available.
For a quote, samples or help building a replacement register for your steam lines, contact the HENGHUA team.
著者について。 HENGHUA’s engineering and test team builds and tests steam hose assemblies, reviews installations in the field, and writes the inspection and maintenance guidance used by distributors and plant maintenance crews. The team works from hydrostatic test benches, assembly records from the steam hose line, and feedback from steam, curing and industrial hose applications.
 English
 Spanish
 Portuguese
 French
 German
 Arabic
 Russian
 Indonesian
 Japanese
 Korean