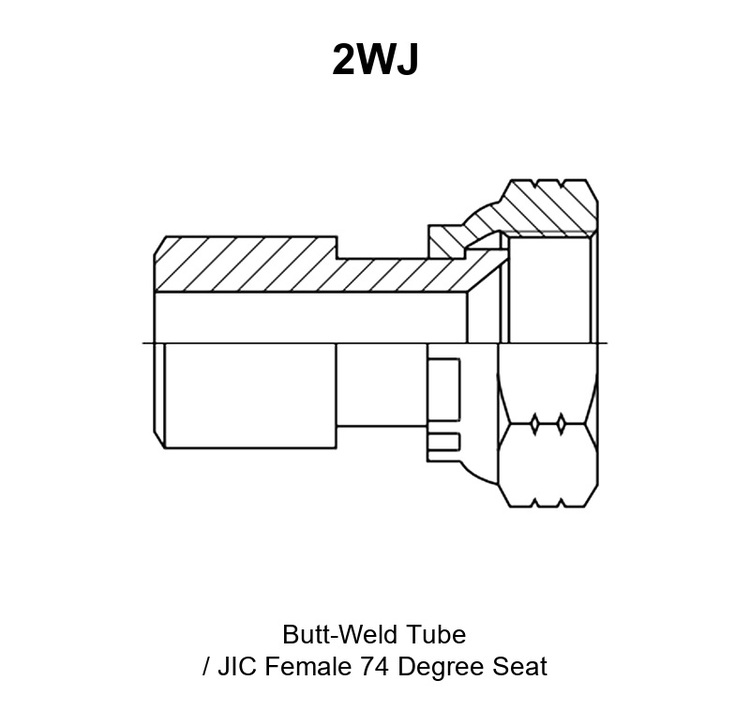
A 2WJ adapter joins a plain butt-weld tube end to a port that accepts a JIC male 74 degree cone stud end. The weld end is joined to the tube by welding rather than by a thread, so the printed table gives a tube outside diameter at that end instead of a thread size. The seat end is a female 74 degree seat and it seals metal-to-metal on the wide cone face of the mating stud end.
Core Advantages
- Weld end accepts a plain tube of a stated outside diameter, so no thread has to be cut on the tube.
- Female 74 degree seat end seals metal-to-metal on the mating male cone, with no O-ring and no thread sealant.
- Nine published rows, covering tubes from 10 mm to 34 mm outside diameter and seat threads from 7/16″X20 to 1.5/8″X12.
- Straight machined body with a wrench hex at the seat end, so the part can be held and aligned while the tube is set up.
- Carbon steel with trivalent chromium zinc plating, or 304 / 316 stainless steel for corrosive and offshore service.
- Turned from bar stock to the series drawing, with thread gauges and dimensional checks applied batch by batch before packing.
1. What a 2WJ Adapter Does
The 2WJ adapter converts a welded tube connection into a JIC female 74 degree seat connection. One end is a plain socket that slips over a tube and is joined to it by welding, and the other end is a female port with an internal thread and a 74 degree cone seat machined inside it. Between the two ends the body is a straight machined bar, so the assembled tube run continues in one line through the adapter.
Both connection ends of every row must match their mating part exactly. The socket has to suit the outside diameter and the wall thickness of the tube being welded, and the thread size, the pitch and the 74 degree seat angle have to agree with the stud end that will be turned into the port. That double match is the precondition for eliminating leakage at the conversion point, and on a welded joint a socket that does not suit the tube wall cannot be welded to the quality the joint needs.
The sealing principle of this series is mixed, and the two ends are read separately. The JIC end is a 74 degree cone metal seat, so it seals by metal-to-metal contact between the wide cone face inside the port and the 74 degree cone of the mating stud end, with no O-ring, no bonded washer and no thread sealant. The weld end does not seal on a thread at all: it seals on a circumferential fusion weld between the tube and the socket wall. Because the tube is welded instead of threaded, this tube adapter carries a TUBE O.D. column in place of a thread column at that end, and that column is read as the size of tube the socket accepts.
2. 2WJ Specifications
2.1 Connection 1 – Butt-weld tube socket, tube outside diameter 10 mm to 34 mm
- Connection type: plain butt-weld socket, machined as a bore that takes the tube end. It is neither a male nor a female thread, because no thread is used at this end.
- Size range available: tubes of 10, 12, 14, 18, 20, 22, 28 and 34 mm outside diameter, as listed in the TUBE O.D. column of section 2.5. The 14 mm tube size is published against two different seat threads, so nine part numbers cover eight tube diameters.
- Gender and interface: socket end, sized to the outside diameter of the tube. Confirm the tube wall thickness and the socket depth against the series drawing before welding.
- Sealing method: circumferential fusion welding of the tube to the socket wall. The joint becomes pressure-tight only after the weld is completed to the procedure selected for the tube material.
- Mating part standard: a plain steel tube, either seamless or welded and drawn, cut square and deburred at the end that enters the socket.
2.2 Connection 2 – JIC female 74 degree seat, internal thread F
- Thread standard and family: SAE J514, SAE 74 degree seat and flareless family. The thread form is the unified fine thread used by the JIC 74 degree cone stud end of the same dash size.
- Thread sizes available at F: 7/16″X20, 1/2″X20, 9/16″X18, 3/4″X16, 7/8″X14, 1.1/16″X12, 1.5/16″X12 and 1.5/8″X12.
- Gender: female adapter thread (internal) with an internal cone seat.
- Sealing method: metal-to-metal contact on the 74 degree cone seat machined inside the port, against the 74 degree cone of the mating male stud end. No O-ring, no bonded washer and no thread sealant is used at the seat.
- Mating port standard: a male 74 degree cone stud end, or a hose end with a 74 degree cone, of the same dash size and thread as F.
- Wrench feature: hex S1 is machined on the body at the seat end, so the adapter can be counter-held while the stud end is tightened.
2.3 Construction and Materials
- Body material: this steel hydraulic adapter is offered in carbon steel, 304 stainless steel, 316 stainless steel or brass, selected per order.
- Plating: trivalent chromium zinc plating (Cr3+) or zinc-nickel plating on carbon steel bodies. Stainless steel bodies are supplied without plating.
- Seat form: the female port is machined with an internal 74 degree cone seat, cut in the same set-up as the thread where the process allows, so the seat runs true to its thread.
- Seal material: this hydraulic adapter carries no elastomeric seal, so there is no elastomer to select at the seat end and none to age. Where an O-ring or a bonded seal is used at another joint in the same circuit, the published material ranges are approximately -30°C to +100°C for NBR, -20°C to +200°C for FKM and -40°C to +120°C for EPDM.
- Machining process: the body is turned from bar stock on CNC lathes, the internal thread and the 74 degree seat are cut, the weld socket bore is machined to the tube diameter, and the part is deburred. Threads are gauged with plug gauges, and the socket bore, the hex and the overall length are checked against the drawing batch by batch before packing.
- Weld-end preparation: the socket bore is supplied clean and free of plating build-up and burrs, so the tube seats to the required depth before welding.
2.4 Pressure and Temperature
Temperature is governed by the body material and by the tube material at the weld end, because this adapter carries no elastomeric seal. A carbon steel body with zinc plating suits general hydraulic service, and 304 or 316 stainless steel is selected for corrosive environments. The body material is normally matched to the tube material rather than chosen independently, so that the welded joint is made between compatible parts.
Working pressure for a given 2WJ adapter size is confirmed per order by HENGHUA engineering, based on the tube outside diameter, the tube wall thickness, the thread size, the sealing method and the material selected. No single pressure figure is published here for a specific size, because a 10 mm tube socket and a 34 mm tube socket do not share one rating. The weld end is usually the limiting end, since the joint quality follows the tube wall and the welding procedure, so the tube specification belongs in the enquiry.
2.5 Part Number and Dimension Table
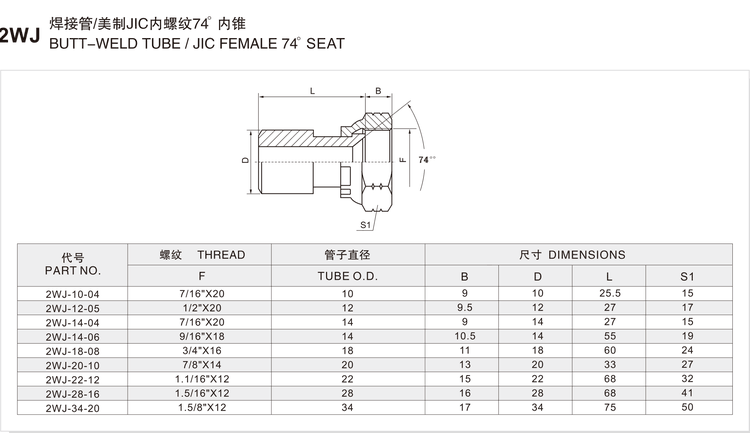
The table below is the complete published dimension table for the 2WJ JIC adapter series. Every row is reproduced in printed column order. The third column is a tube outside diameter and not a thread size, because the weld end is joined to the tube by welding rather than by a thread.
| PART NO. | F | TUBE O.D. | B | D | L | S1 |
|---|---|---|---|---|---|---|
| 2WJ-10-04 | 7/16″X20 | 10 | 9 | 10 | 25.5 | 15 |
| 2WJ-12-05 | 1/2″X20 | 12 | 9.5 | 12 | 27 | 17 |
| 2WJ-14-04 | 7/16″X20 | 14 | 9 | 14 | 27 | 15 |
| 2WJ-14-06 | 9/16″X18 | 14 | 10.5 | 14 | 55 | 19 |
| 2WJ-18-08 | 3/4″X16 | 18 | 11 | 18 | 60 | 24 |
| 2WJ-20-10 | 7/8″X14 | 20 | 13 | 20 | 33 | 27 |
| 2WJ-22-12 | 1.1/16″X12 | 22 | 15 | 22 | 68 | 32 |
| 2WJ-28-16 | 1.5/16″X12 | 28 | 16 | 28 | 68 | 41 |
| 2WJ-34-20 | 1.5/8″X12 | 34 | 17 | 34 | 75 | 50 |
What each column means:
- PART NO. is the ordering code. The two numbers after the prefix give the tube outside diameter in millimetres and the dash size of the seat thread, in that order.
- F is the internal thread at the JIC female 74 degree seat end, in catalogue notation. The number after X is the pitch in threads per inch, so 9/16″X18 is a 9/16″ unified fine thread at 18 threads per inch.
- TUBE O.D. is the nominal outside diameter of the tube that the weld end accepts, in millimetres. It is a tube size, not a thread size.
- B is a body dimension in millimetres, marked B on the series drawing. Confirm the reference points against that drawing when the space around the tube run is tight.
- D is the tube outside diameter as called out on the series drawing, in millimetres. It carries the same value as the TUBE O.D. column in every published row.
- L is the overall length of the adapter in millimetres.
- S1 is the width across flats of the hex on the body, in millimetres. It is a wrench size, not a thread size.
Thread size and dash chart for the seat end:
| Dash code | Nominal size | JIC thread F | Tube O.D. (mm) in the matching rows | S1 (mm) |
|---|---|---|---|---|
| -04 | 1/4″ | 7/16″X20 | 10, 14 | 15 |
| -05 | 5/16″ | 1/2″X20 | 12 | 17 |
| -06 | 3/8″ | 9/16″X18 | 14 | 19 |
| -08 | 1/2″ | 3/4″X16 | 18 | 24 |
| -10 | 5/8″ | 7/8″X14 | 20 | 27 |
| -12 | 3/4″ | 1.1/16″X12 | 22 | 32 |
| -16 | 1″ | 1.5/16″X12 | 28 | 41 |
| -20 | 1.1/4″ | 1.5/8″X12 | 34 | 50 |
3. How to Read a 2WJ Part Number
Every 2WJ adapter part number has three parts: the series prefix, the tube size and the seat dash size.
- 2WJ is the series prefix. It identifies the part of this page: a straight tube adapter that welds to the tube on one side and carries a JIC female 74 degree seat on the other.
- The first number after the prefix is the tube outside diameter in millimetres, so 14 in 2WJ-14-06 means a 14 mm tube.
- The second number is the dash size of the JIC seat thread, following the SAE J514 dash convention in which the number is the nominal tube outside diameter in sixteenths of an inch. 04 means 1/4″, 05 means 5/16″, 06 means 3/8″, 08 means 1/2″, 10 means 5/8″, 12 means 3/4″, 16 means 1″ and 20 means 1.1/4″.
- The dash size fixes the thread, so 2WJ-12-05 carries a 1/2″X20 seat thread, which is the thread used by the 5/16″ dash in the 74 degree seat family.
- No suffix is applied to any row in the 2WJ table. Other series in the same catalogue use suffixes such as -SP, -WD or -PK to mark a variant; if a suffix appears on your drawing, quote the full part number including it.
Worked example using a real row of the table. Part number 2WJ-14-06 decodes as follows:
- Series: 2WJ, butt-weld tube to JIC female 74 degree seat adapter.
- Weld end: a socket for a 14 mm outside diameter tube, marked TUBE O.D. 14 and D 14.
- Seat end F: 9/16″X18 internal thread with a 74 degree cone seat, the dash 06 size of the 74 degree seat family.
- Body dimension B: 10.5 mm, overall length L: 55 mm, wrench hex S1: 19 mm.
4. Installation and Fitment
A 74 degree seat joint is made by drawing the male cone into the female seat until the two metal faces meet. Tightening is a feel-and-angle operation rather than a flat torque figure: bring the stud end in finger-tight, snug it with a wrench, and continue only as far as the port specification requires. Once the cone is fully seated, no further tightening improves the seal; it only loads the thread and the body.
The weld end is a different operation and decides most of the quality of the assembly. Cut the tube square, deburr it inside and outside, and clean the tube end and the socket bore of oil, scale and plating debris. Insert the tube to the socket depth shown on the series drawing, align the run, tack the joint, and complete the weld to the procedure selected for the tube material. Let the assembly cool before the JIC stud end is fitted, and shield the seat end from weld heat and spatter.
Keep the seat face clean and free of burrs, spatter and old sealant. A 74 degree seat seals on a machined cone face, and a single nick or a trapped chip will produce a weep that no amount of tightening will remove. Do not apply PTFE tape or liquid sealant to the cone face of the stud end, because a film of sealant will hold the cone off its seat.
Assembly steps:
- Confirm that the tube to be welded is the outside diameter printed in the TUBE O.D. column for the part number selected, and that its wall thickness suits the socket.
- Confirm that the mating stud end is a male 74 degree cone of the same dash size and thread as F, and that it is not a 37 degree flare or an O-ring boss.
- Cut the tube square, deburr it, and clean the tube end, the socket bore and the seat face.
- Fit the tube into the socket to the drawing depth, align the run, and tack the joint.
- Complete the weld to the procedure selected for the tube material, shield the seat end, and let the assembly cool.
- Turn the JIC stud end in by hand, snug it with a wrench while holding S1, then leak-check the assembly at the pressure agreed for the system.
Common fitment errors and their symptoms:
- Welding a tube of the wrong outside diameter into the socket. The symptom is an oversized gap and a joint that weeps at the weld line.
- Welding with a stud end already tightened into the seat. The symptom is a distorted cone seat and a seat-end weep as soon as the circuit is pressurised.
- Fitting a 37 degree flared hose end into the 74 degree seat port. The two angles differ, no full metal-to-metal contact is generated, and the joint weeps from the first pressurisation.
- Over-tightening to stop a seat weep. The symptom is a stretched thread or a distorted seat, because the metal faces are already in contact.
5. Applications and Industries
Application tags for this hydraulic adapter: hydraulic systems, water jetting, oil and gas, industrial equipment, construction machinery, agriculture, marine and material handling.
Concrete scenarios where a 2WJ adapter earns its place:
- Fabricated tube runs in OEM assembly. A machine builder who bends and welds steel tube for a pressure line can end that line in a 74 degree seat port without threading the tube, so the tube shop and the hose shop never have to agree on a thread at the tube.
- Repair of a welded tube assembly. Where a welded tube end has been cut back or a socket has been damaged, a replacement adapter can be welded on and the seat end reused with the original hose assembly, provided the tube diameter and the seat thread still match.
- Test benches and rigs. A bench plumbed in welded tube on the supply side and in JIC 74 degree seat hose ends on the test side uses this 2WJ adapter fitting at the transition.
- Cross-standard equipment integration. Where a machine uses metric tube outside diameters, the metric sizes in this table allow a welded metric tube to be terminated in the SAE J514 74 degree seat family used by the rest of the circuit.
The same part suits fluid power circuits, agricultural implement hydraulics, marine deck equipment, construction machinery and material handling systems, supplied as a steel hydraulic adapter in carbon steel with zinc plating or in 304 / 316 stainless steel for offshore and coastal service.
6. Replacement and Cross-Reference Guide
Replacement selection for this steel hydraulic adapter is organised by thread standard and sealing method, never by brand or catalogue number. This 2WJ adapter is identified by three measurements, and nothing else is needed to find a matching part in the table.
Measure these three things:
- Measure the tube outside diameter and the tube wall thickness. The outside diameter has to equal the TUBE O.D. value of the row you choose, and the wall thickness decides whether the socket is suitable and how the joint is welded. A 10 mm tube and a 34 mm tube are not interchangeable in any respect.
- Measure or identify the seat thread. Thread diameter and pitch in threads per inch must agree with the F column, so a 9/16″X18 port calls for a row with F 9/16″X18. Check the angle as well, because a 74 degree seat is a wide cone seat and not the same joint as a 37 degree flare.
- Confirm the end configuration. This JIC adapter is a welded tube end on one side and a female 74 degree seat on the other, in a straight body. It does not replace a male-to-male adapter, an elbow or a tee, and it does not replace a series whose tube end is threaded and uses a nut and sleeve instead of a weld.
Series that are commonly confused with 2WJ and are not interchangeable: the SAE J514 JIC 37 degree flare family, which seals on a conical flare face of a different angle; the SAE J1926-3 / ISO 11926-3 O-ring boss family, which seals with an O-ring on a straight-thread stud end plus a lock nut; the SAE J1453 ORFS family, which seals on a flat face against an elastomeric O-ring; and the NPT and BSPT tapered pipe thread families, which seal on the thread flanks and need a sealant.
7. Ordering, Packaging and Delivery
To order this tube adapter from the 2WJ series, give the series code plus the full part number, for example 2WJ-14-06, and confirm the following with the enquiry:
- Full part number, including any suffix shown on your drawing or packing list.
- Tube outside diameter and wall thickness, so the socket and the weld preparation can be checked against the drawing.
- Body material: carbon steel, 304 stainless steel, 316 stainless steel or brass.
- Plating for carbon steel bodies: trivalent chromium zinc plating (Cr3+) or zinc-nickel plating.
- Quantity and the required delivery date.
Parts are packed in labelled bags or boxes carrying the full part number, with cartons marked for size and quantity, and the seat end protected so the cone face arrives free of nicks. Packaging is arranged for distributor shelves and for direct-to-line OEM delivery. Sample orders and mixed-size trial orders are accepted before a production release, and custom sizes, specials and drawing-based manufacture can be quoted for OEM programmes, including tube diameters outside the published rows. Lead time is confirmed per order.
8. FAQ
What is the difference between JIC 37° flare and ORFS, and which should I use? A JIC 37° flare fitting seals metal-to-metal on a conical flare face and is specified by SAE J514 in the SAE 37° flared family. An ORFS fitting, specified by SAE J1453, seals on a flat face against an elastomeric O-ring held in a groove. Use the family that matches the port on your equipment. Neither one is a substitute for the seat end of this adapter, which has a 74 degree cone seat.
Can NPT and BSPT be interchanged? No. NPT is an American tapered pipe thread made to ANSI/ASME B1.20.1, and BSPT is a British tapered pipe thread made to ISO 7-1. They differ in thread form and pitch, so the same nominal size will often start by hand and then bind, and the joint will weep. Where a pipe thread has to meet the 74 degree seat end, use an adapter that converts between the two families.
How do I identify the correct 2WJ adapter size? Read the two numbers in the part number separately. The first number is the tube outside diameter in millimetres and has to match the tube you will weld; the second is the JIC dash size and has to match the thread you will connect to, so 2WJ-14-06 is a 14 mm tube with a 9/16″X18 seat. Measure both, then check S1 and L against the space available around the tube run.
What seal material should I select for my fluid and temperature? This JIC adapter has no elastomeric seal at either end, because the seat end is a metal-to-metal 74 degree cone joint and the tube end is a weld, so the decision here is the body and the plating. Carbon steel with trivalent chromium zinc plating suits general hydraulic service, and 304 or 316 stainless steel is selected for corrosive environments. Where an elastomer is used elsewhere in the same circuit, the published ranges are approximately -30°C to +100°C for NBR, -20°C to +200°C for FKM and -40°C to +120°C for EPDM.
How is the working pressure of this adapter determined? Working pressure is confirmed per order by HENGHUA engineering, based on the tube outside diameter, the tube wall thickness, the thread size, the sealing method and the material selected. Because a 10 mm tube socket and a 34 mm tube socket do not share one rating, no single figure is published for the whole series. The welded joint is part of that review, since its strength follows the tube wall and the welding procedure used.
What is the minimum order quantity and can I get samples? Sample orders and mixed-size trial orders are accepted for validation before a production release. Minimum order quantity depends on the size, the material and the plating selected, and it is confirmed with the quotation.
Is the weld end threaded, or does it use a nut and a sleeve? It is neither. The weld end is a plain socket machined to the tube outside diameter printed in the TUBE O.D. column, and the tube is joined to it by welding. No thread is cut on the tube and no nut or sleeve is used at that end. A nut and sleeve arrangement belongs to a flareless tube connection at a stud end, not to this socket.
Send the full 2WJ adapter part number, the tube outside diameter and wall thickness, the seat thread and the quantity you need, and HENGHUA will confirm the drawing, the material and the lead time with the quotation.
Related series in the same family: the 1J adapter (straight) and the 2J adapter (straight). Browse the full Hydraulic Adapters range for the complete SAE J514 JIC, NPT, ORFS and ISO 6162 flange families.


 English
 Spanish
 Portuguese
 French
 German
 Arabic